Regenerative Thermal Oxidizers
Energy Recovery and Emissions Control with Regenerative Thermal Oxidisers

Engineered for VOC destruction at scale
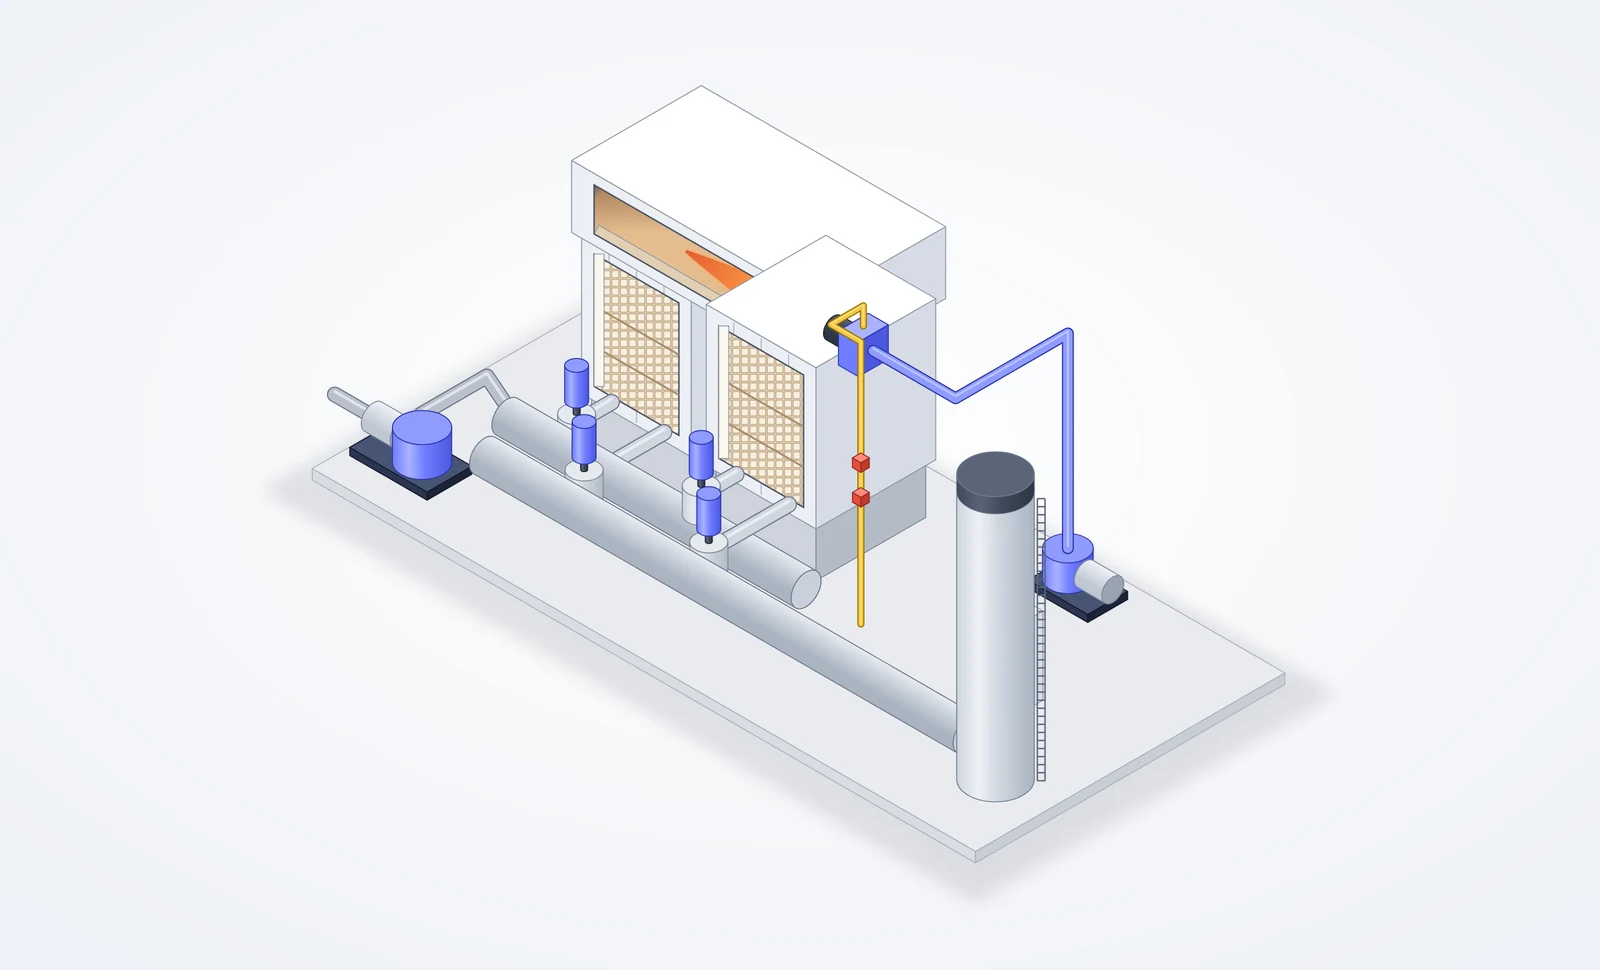
Our Regenerative Thermal Oxidiser (RTO) uses two or three ceramic media beds to capture and recycle up to 95% of exhaust heat while achieving 99% to 99.99% destruction of volatile organic compounds (VOCs) and hazardous air pollutants (HAPs). This energy-efficient design minimises fuel consumption and operating costs, delivering reliable, continuous emissions control for a wide range of industrial processes.
Heat Recovery
Up to 95%
VOC Destruction
99% to 99.99%
Design and build
In-house
Thermal Efficiency
Up to 95%
What is a Regenerative Thermal Oxidizer?
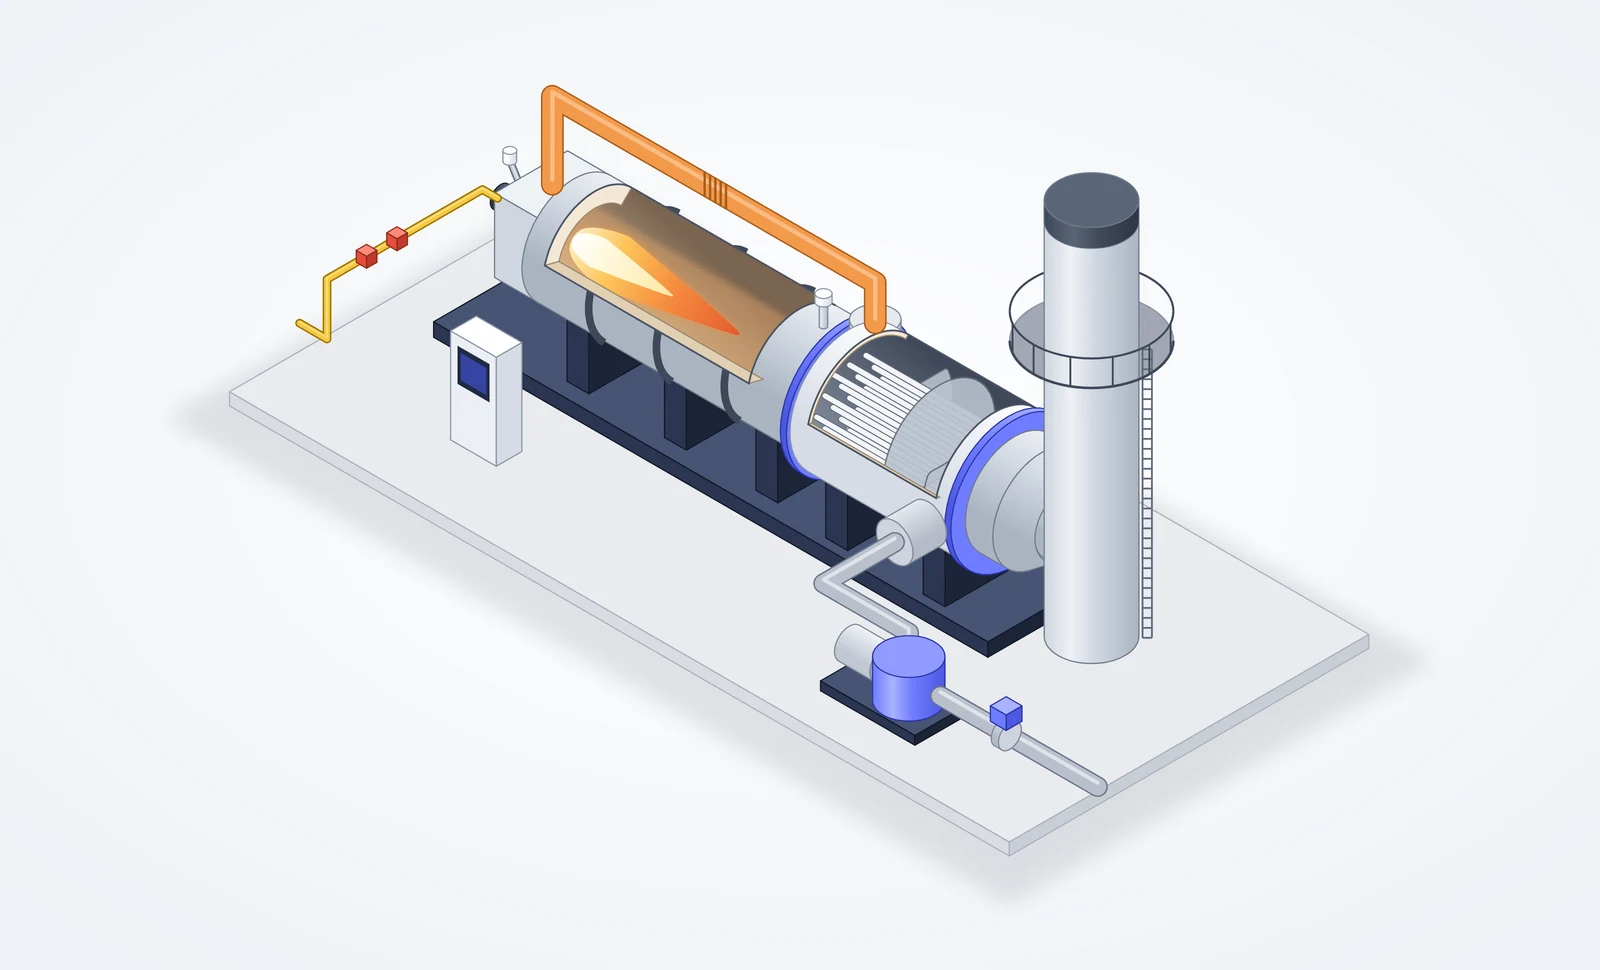
A regenerative thermal oxidiser (RTO) destroys volatile organic compounds and hazardous air pollutants by oxidising them at high temperature, while ceramic media beds recover and reuse the process heat.
How it works
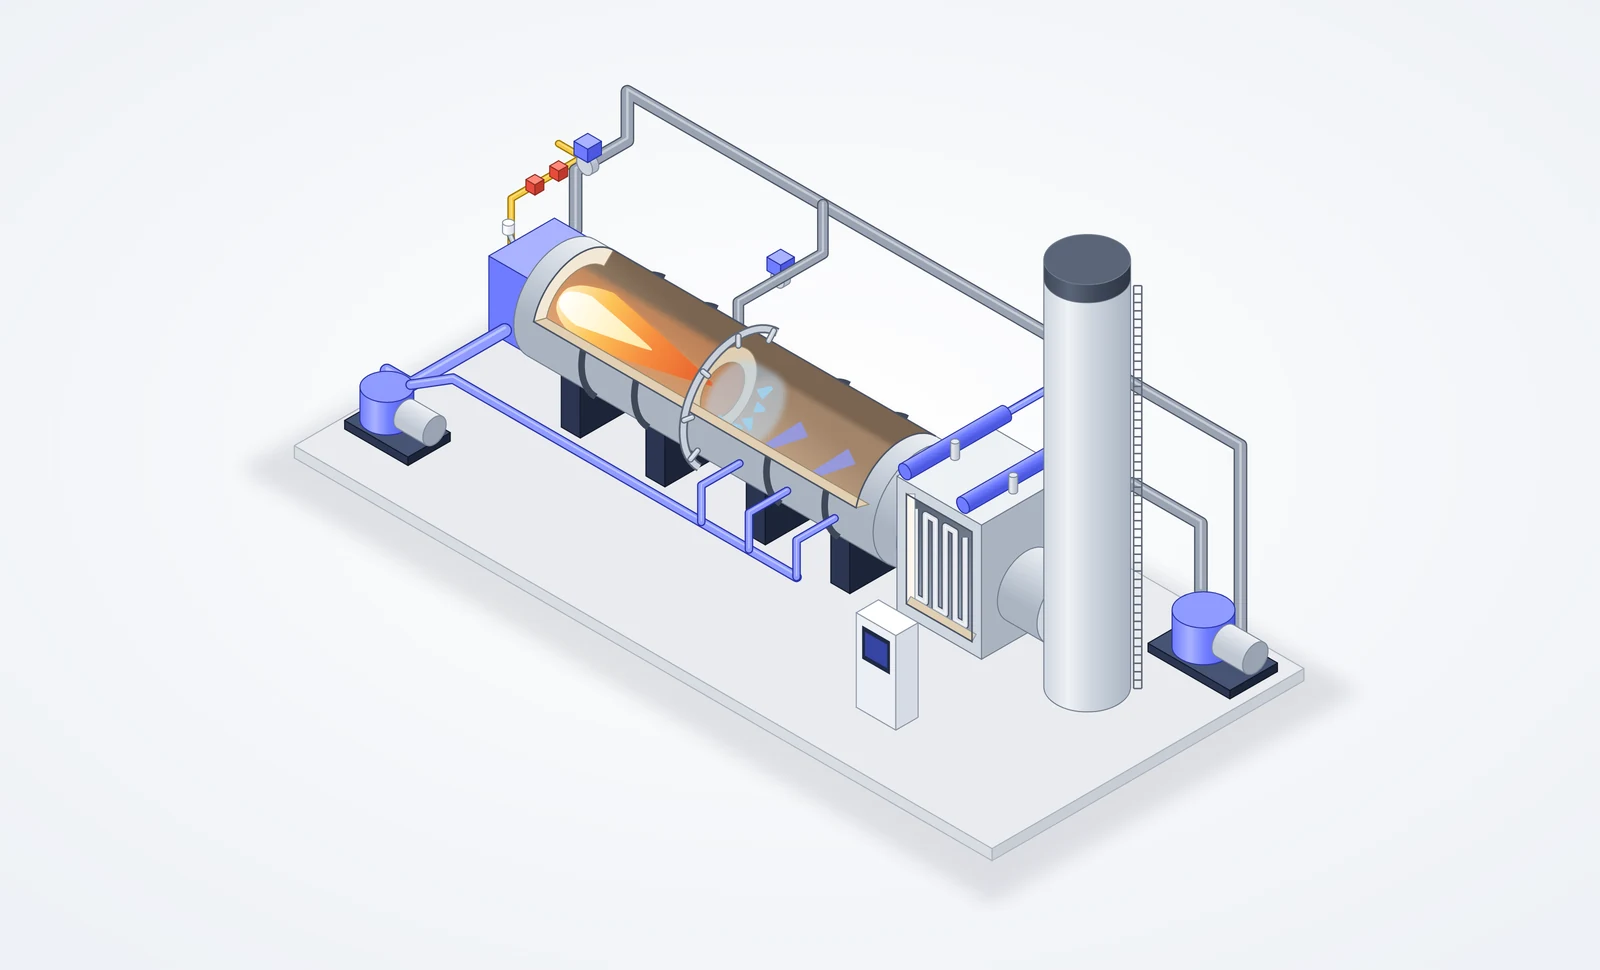
A regenerative thermal oxidiser runs process gas through two ceramic media beds that alternate roles on a timed cycle, one preheating incoming gas while the other captures heat from the outgoing exhaust.
Incoming process gas enters through a ceramic bed already holding heat from the previous cycle, raising the gas to near combustion temperature before it reaches the chamber.
The preheated gas burns in the central combustion chamber, where VOCs and other pollutants oxidise and break down.
Hot exhaust gas passes through the second ceramic bed, depositing combustion heat into the media for use in the next cycle.
Once the second bed has absorbed sufficient heat, a valve reverses gas flow direction so the two beds swap roles, sustaining continuous preheating and heat recovery.
Key Benefits
Recovers up to 95% of energy from exhaust gases, reducing auxiliary fuel needs.
Minimal fuel usage and automated controls drive down lifetime operating expenses.
Fast media bed switching for smooth turndown and stable performance during process variations.
Preheated inlet gas stabilises combustion temperatures, extending refractory life.
Detailed CFD, process simulations, and strict QC are used to achieve adequate residence times and high DRE
The CRA Edge
30+ years of expertise solving the toughest emissions challenges
End-to-end design, R&D, and manufacturing under one roof for speed and quality
ISO 9001 certified; designs aligned with ASME, API and CE
Customised designs engineered for your process needs and the applicable regulations
Applications

Built to help you specify.
Sizing tools, decision guides, and technical references. Use them before, during, and after your evaluation.




Frequently Asked Questions
How much energy does an RTO recover?
A regenerative thermal oxidiser (RTO) recovers up to 95% of the exhaust heat in ceramic media beds, which cuts auxiliary fuel demand in continuous duty. Hot exhaust stores its heat in one ceramic bed, automated valves reverse the flow every 2 to 4 minutes, and the incoming waste gas picks up that stored heat before the combustion chamber, so only make-up heat is needed. The design basis on this page cites autothermal operation once the VOC concentration exceeds 1 to 2% LEL, fuel savings of 60 to 90% against a direct fired unit, and payback depends on fuel price, run hours and the local carbon or flaring penalty regime.
How does an RTO handle variable process loads?
An RTO handles flow variation with modulating dampers that adjust the flow distribution, variable frequency drives on the blowers that match system capacity to demand, a bypass for extreme upsets and fast bed switching that holds thermal efficiency during turndown. Changes in VOC concentration are handled by automatic fuel modulation, temperature control loops and the thermal mass of the ceramic beds, which buffers short swings. For intermittent or batch operation the unit has a quick heat-up sequence, programmed purge cycles for safe shutdown and a hold mode that keeps the beds warm during short stoppages. CRA designs the valve sequencing and controls for the actual load profile of the plant.
Can an RTO be retrofitted to an existing plant?
Yes. An RTO can be retrofitted to an existing operation, and several factors need to be checked first. An RTO has a larger footprint than a direct fired unit, and the weight of the ceramic media needs an adequate foundation. Ductwork must be modified for the inlet and outlet connections and isolation dampers, utilities such as natural gas, electrical power and compressed air may need upgrading, and the unit must be tied into the existing process controls. CRA assesses these points from a site survey and the process data, lays out the unit against the available space and reviews the tie-in sequence with the plant.
What destruction efficiency does an RTO achieve?
A properly designed RTO achieves destruction efficiency of 99% to 99.99% for VOCs and HAPs across a wide range of industrial waste gas applications, which is the design basis on this page. The RTOs CRA manufactures hold this performance through temperature control in the combustion chamber, enough residence time at that temperature, ceramic bed design for uniform heat distribution, flow distribution that treats the whole gas stream, and automated valve sequencing for consistent thermal cycling. Destruction efficiency stays stable across the range of VOC concentrations and flow rates the unit is designed for, including process upsets within that envelope.
How does an RTO compare with a recuperative or direct fired thermal oxidiser?
An RTO recovers up to 95% of the exhaust heat, has the highest capital cost and the largest footprint, and is the right choice for high-flow continuous operation where fuel cost dominates lifecycle economics. A recuperative thermal oxidiser recovers 40 to 70% of the heat through a metal heat exchanger, costs less and takes less space, and suits steady continuous flows where an RTO cannot be justified. A direct fired thermal oxidiser has no heat recovery, the lowest capital cost and the simplest design, and suits high-VOC, intermittent or emergency vent duty. CRA manufactures all three and selects on flow, VOC concentration, operating hours, space and fuel cost.