Purpose Engineered Gas Systems
Projects around the world
Selected case studies across oil and gas, biogas, and emissions control.
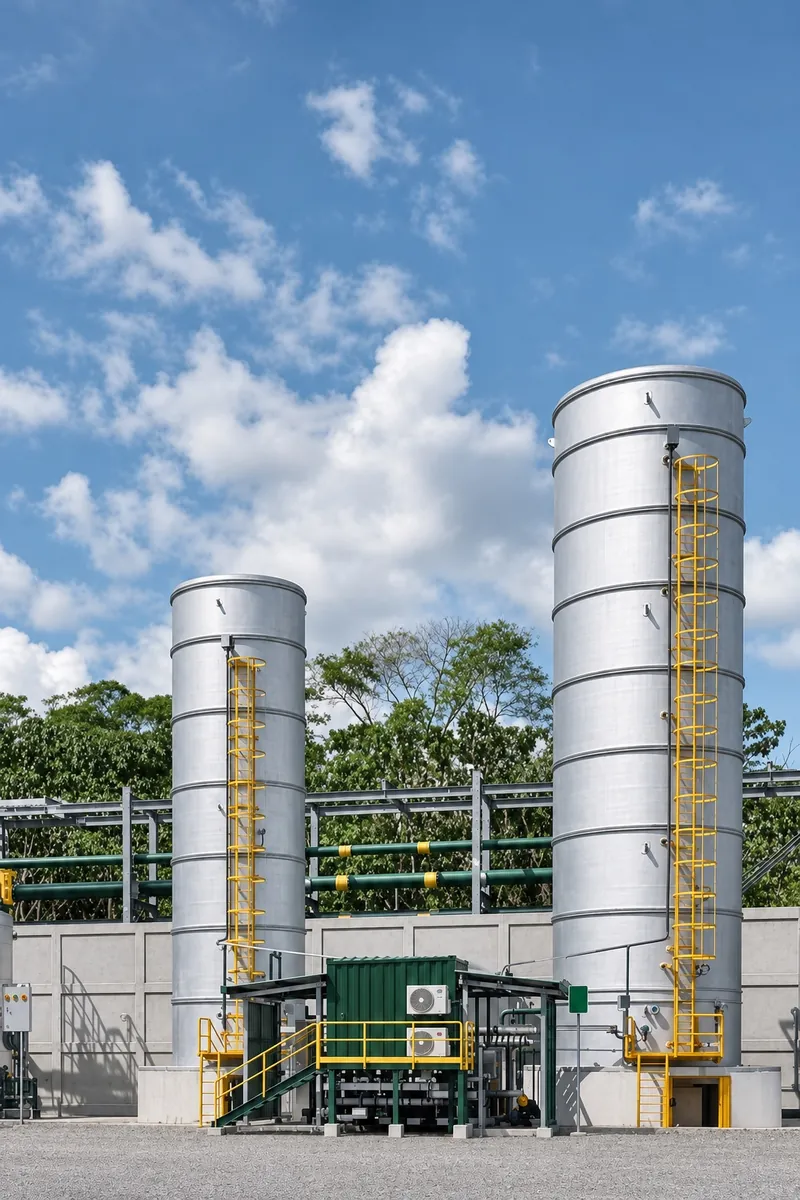
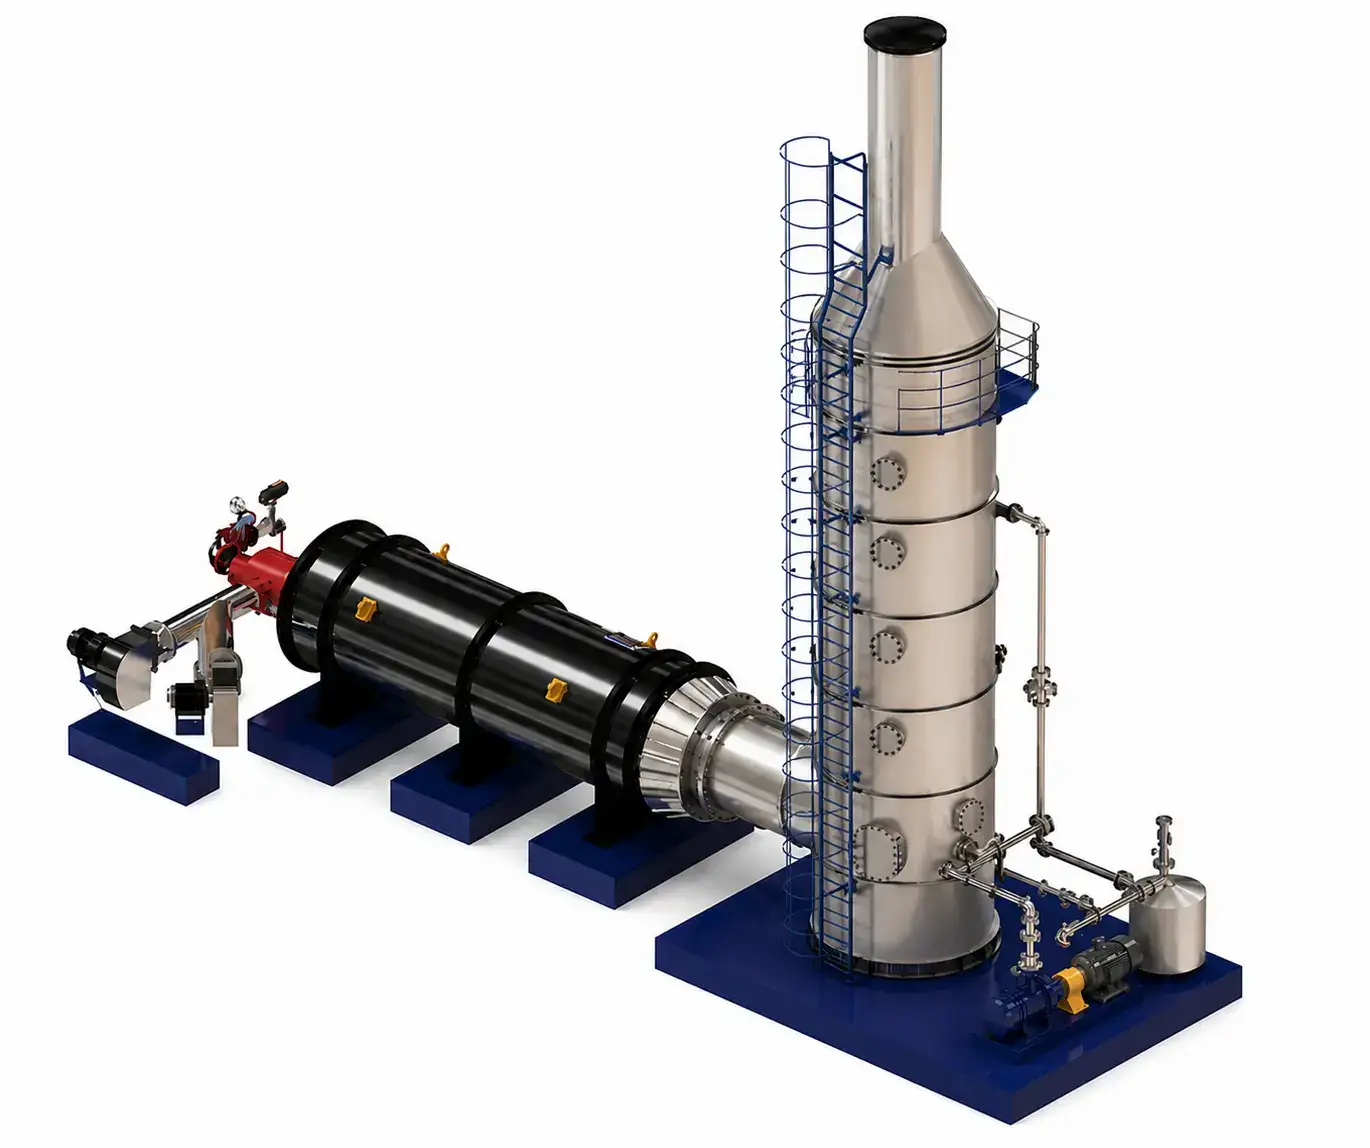
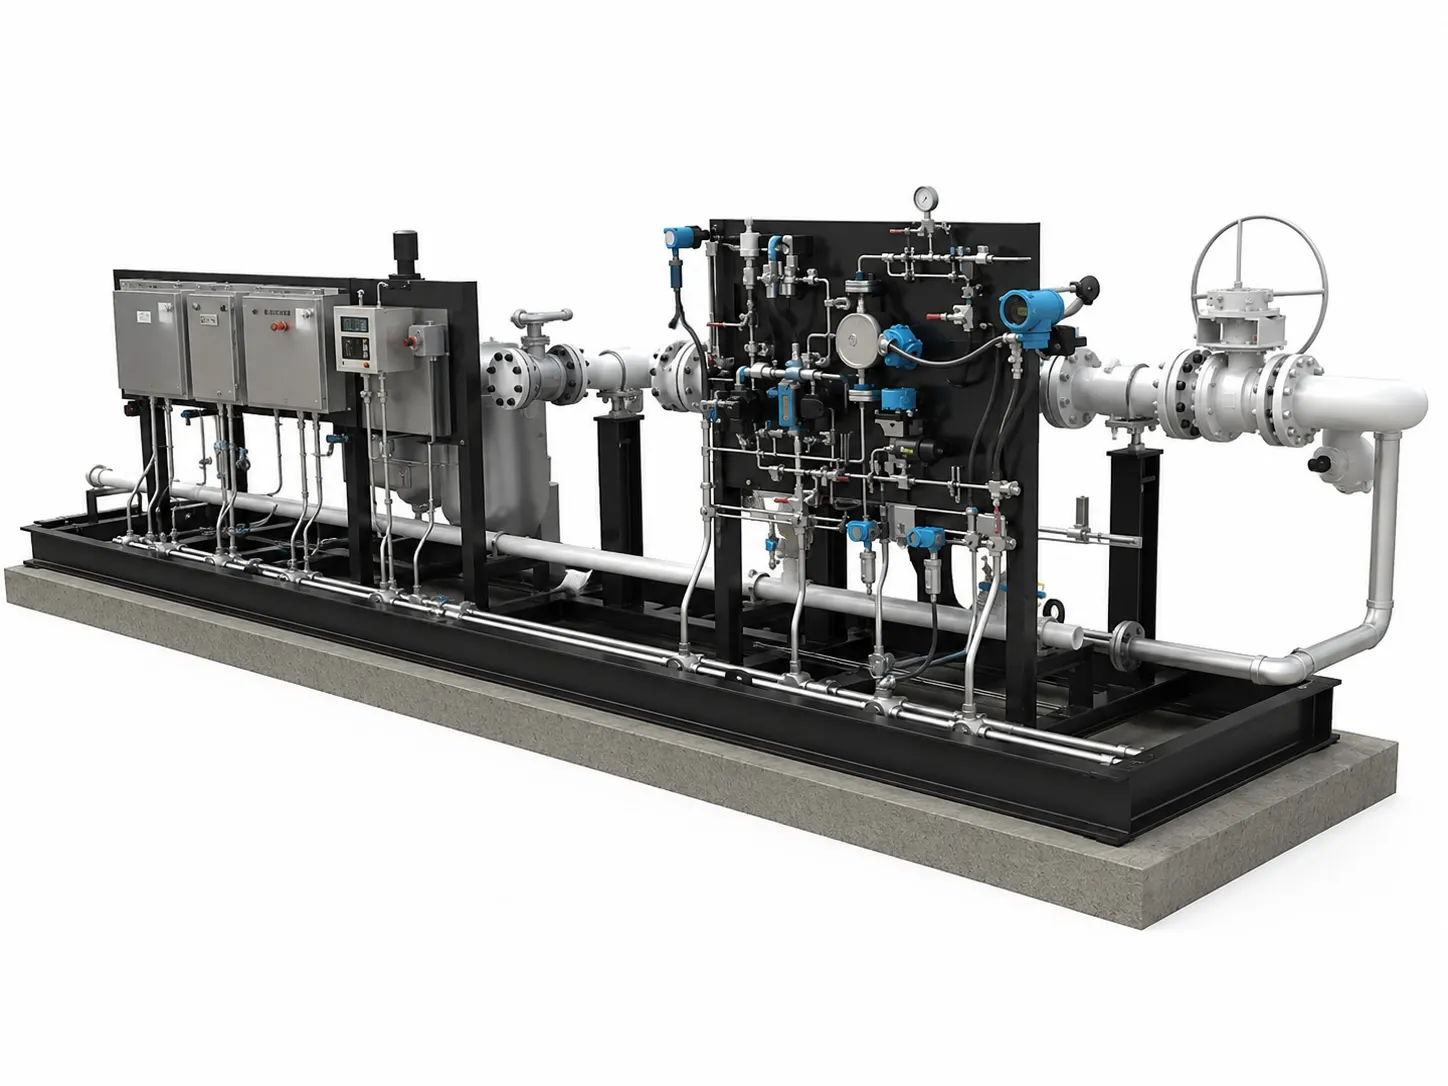
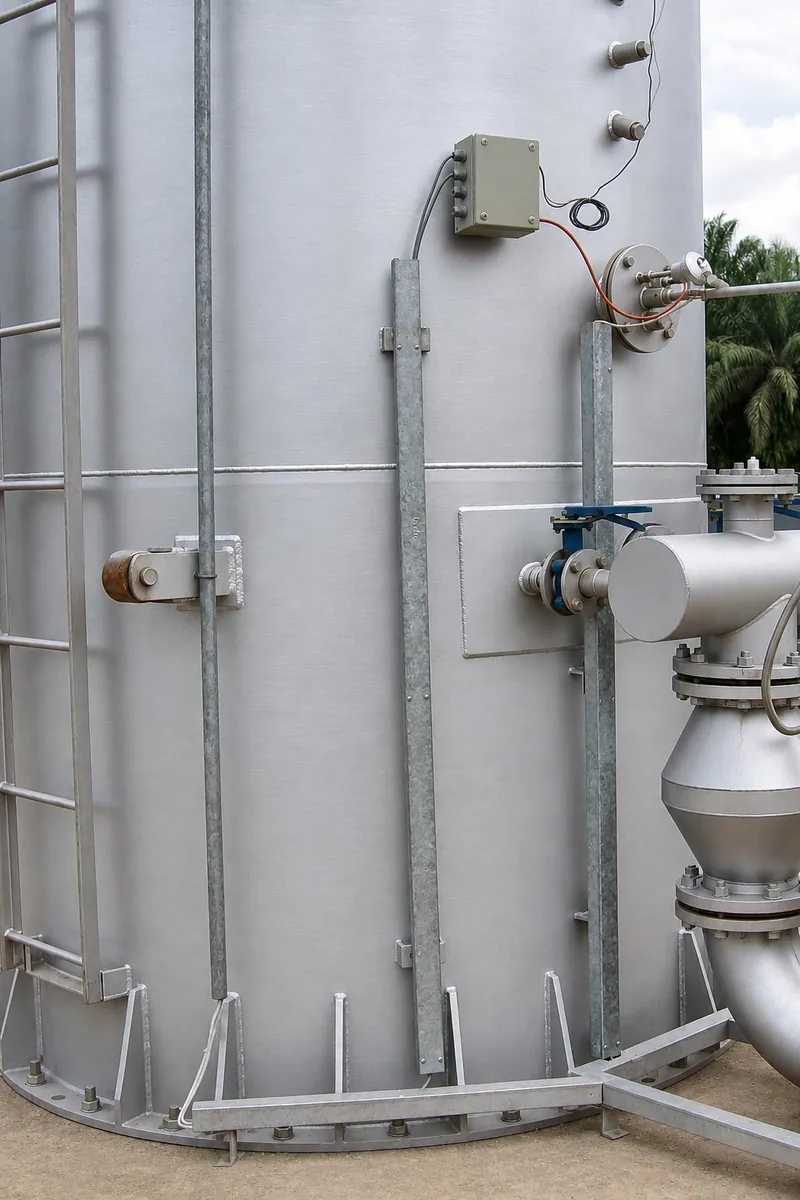
Single enclosed flare for HP and LP associated gas, designed to meet the site's radiation, noise and emission limits.
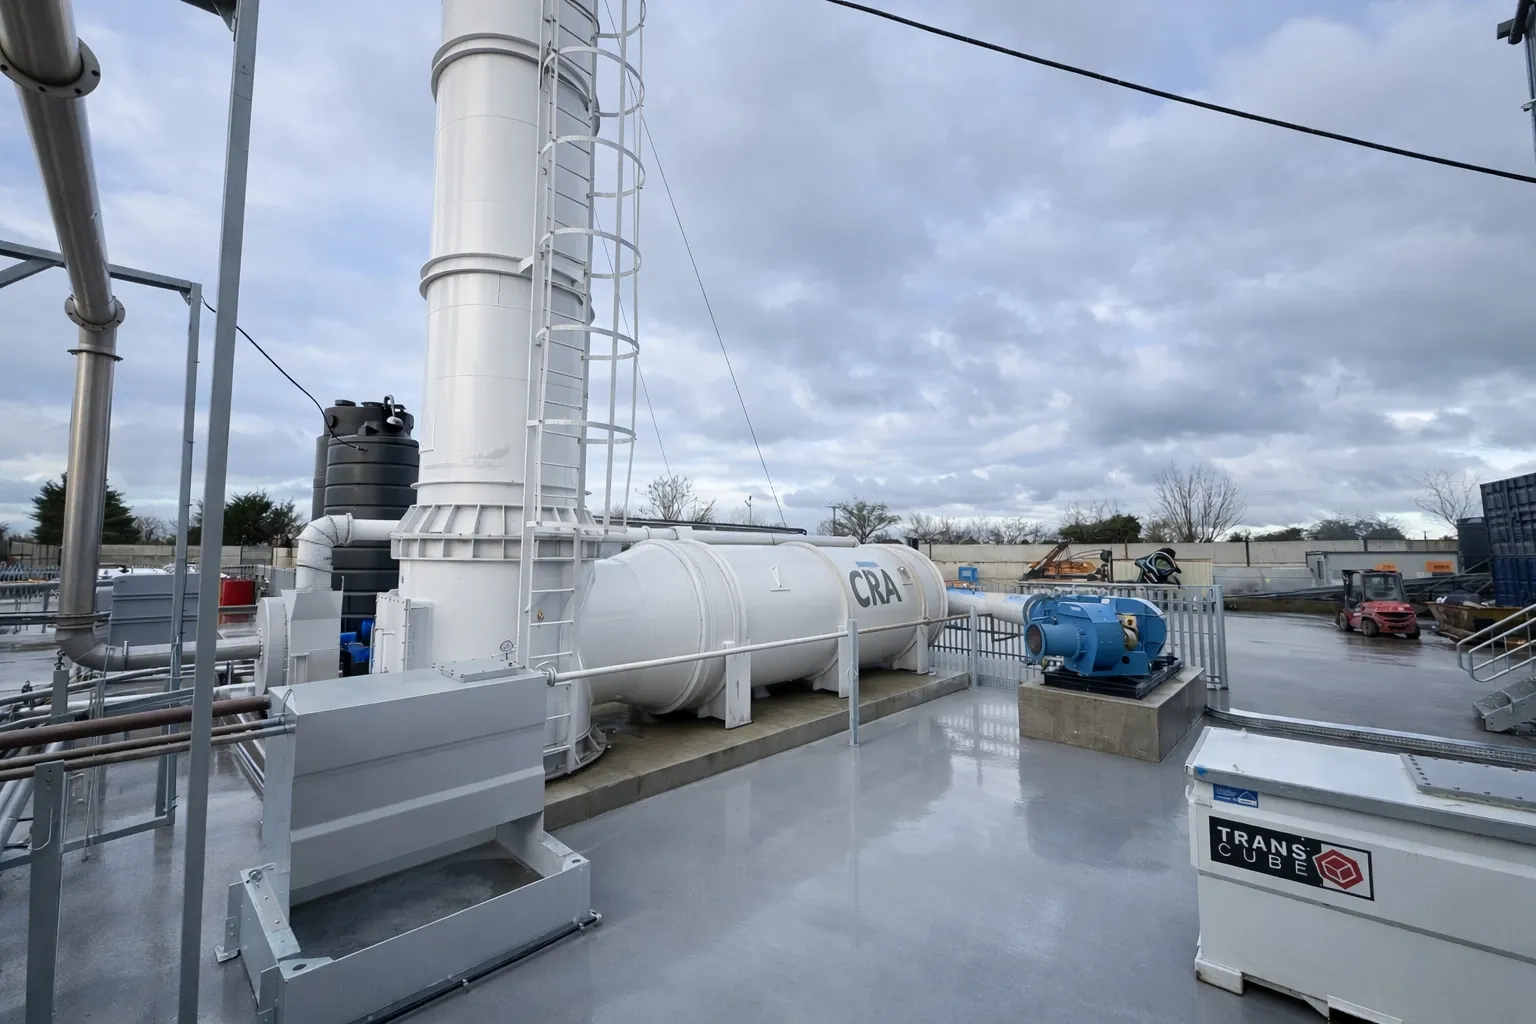
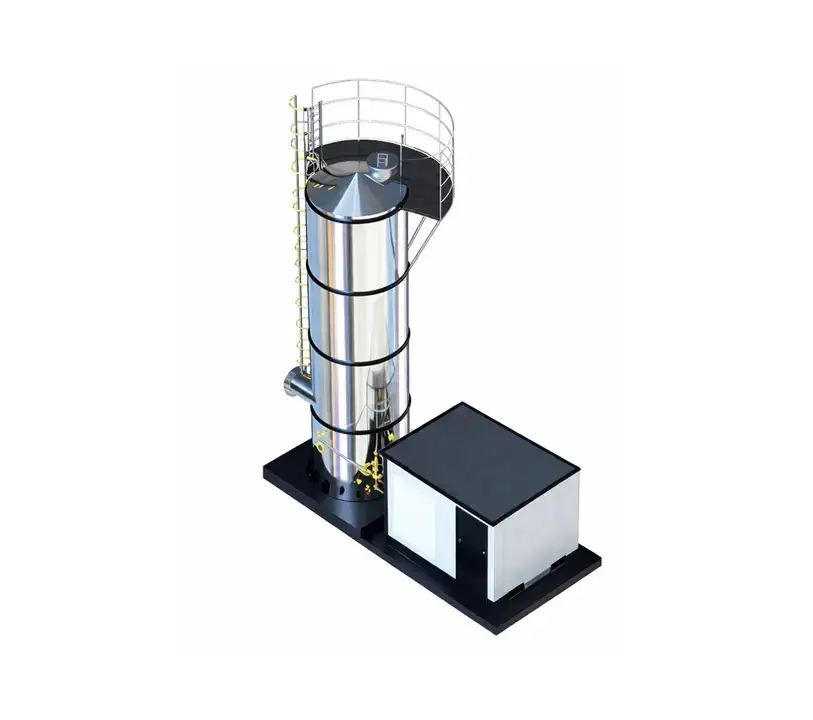
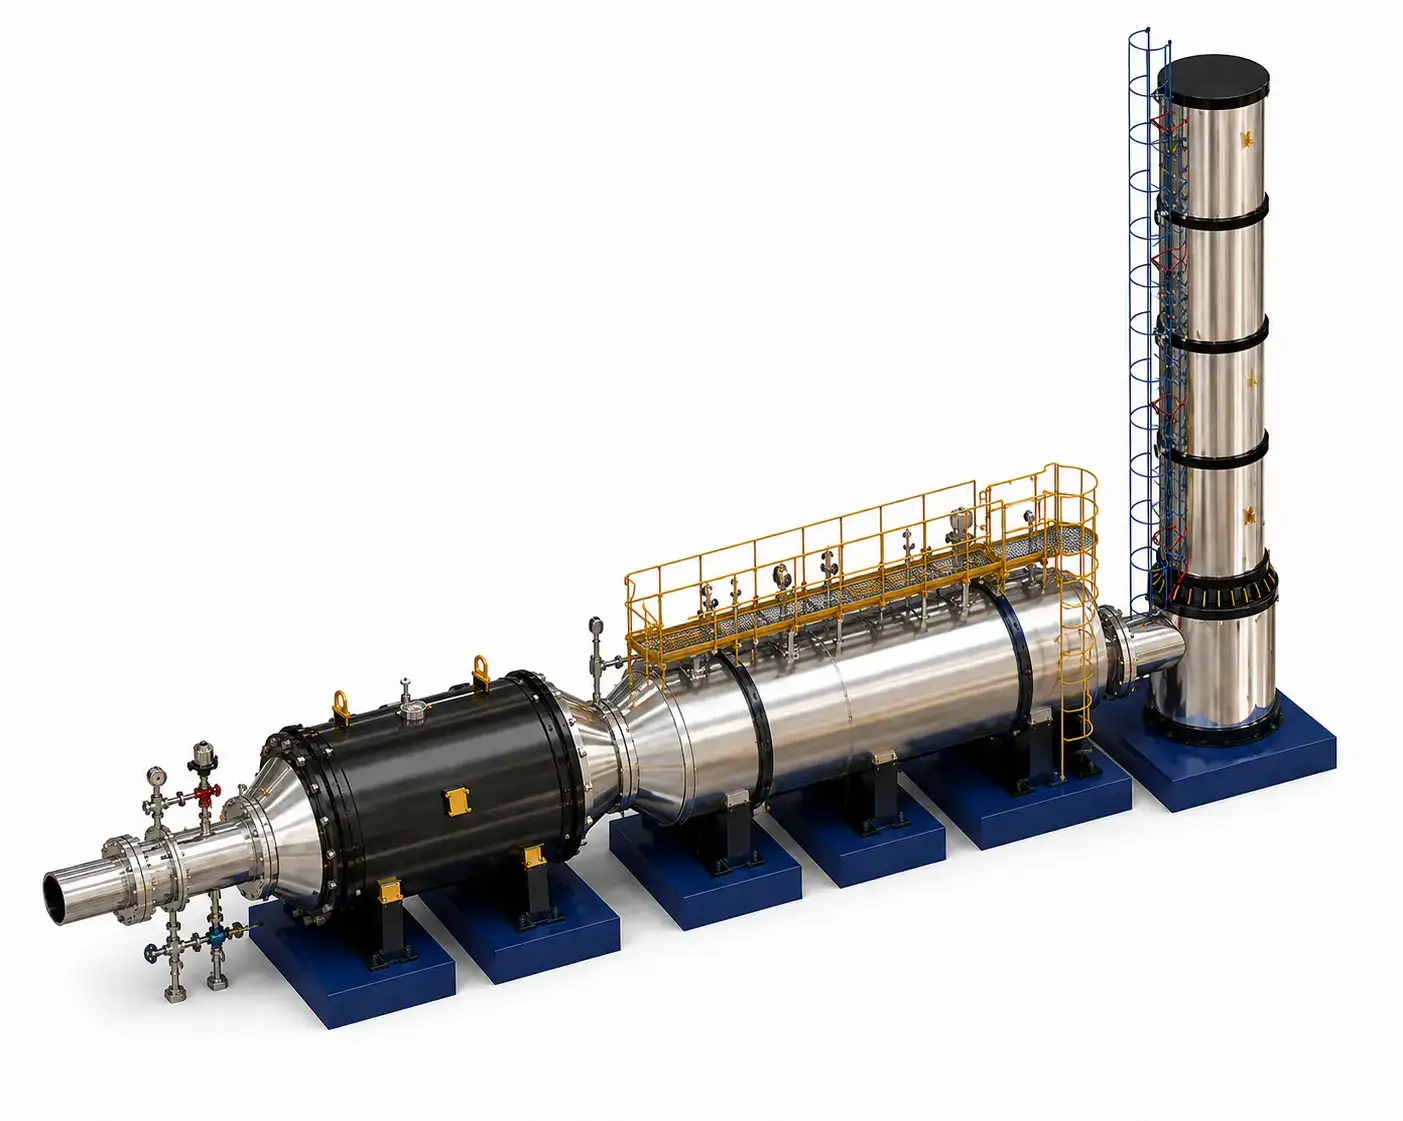
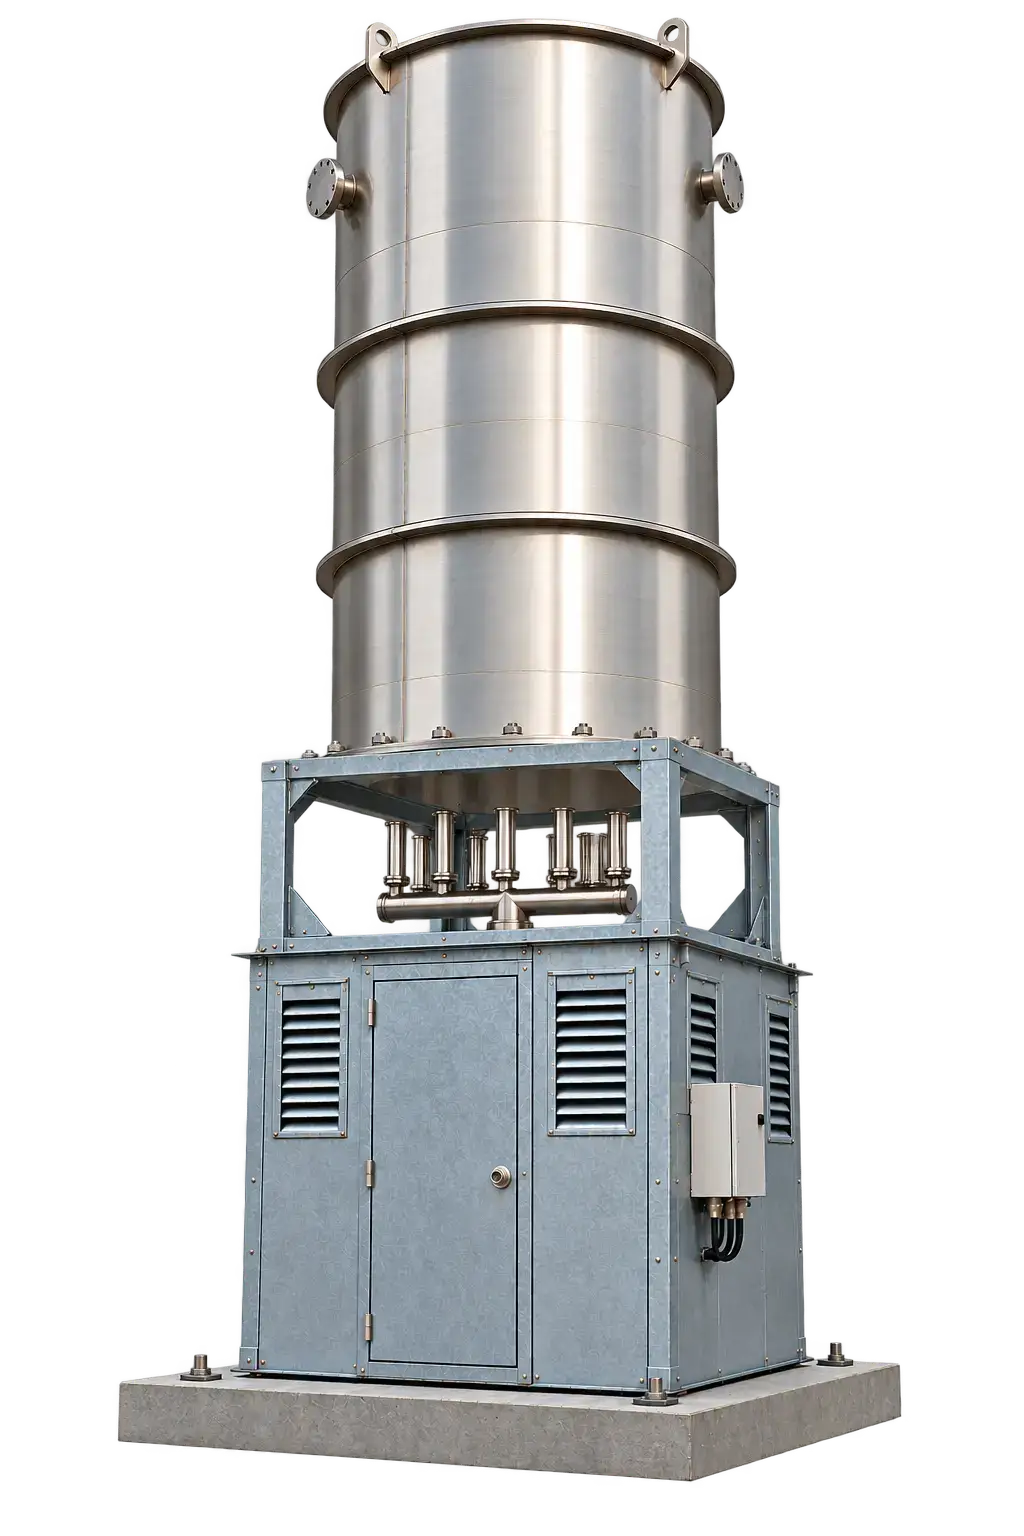
Skid-mounted thermal oxidiser for lean, VOC-laden pyrolysis off-gas, designed in line with UKCA requirements.
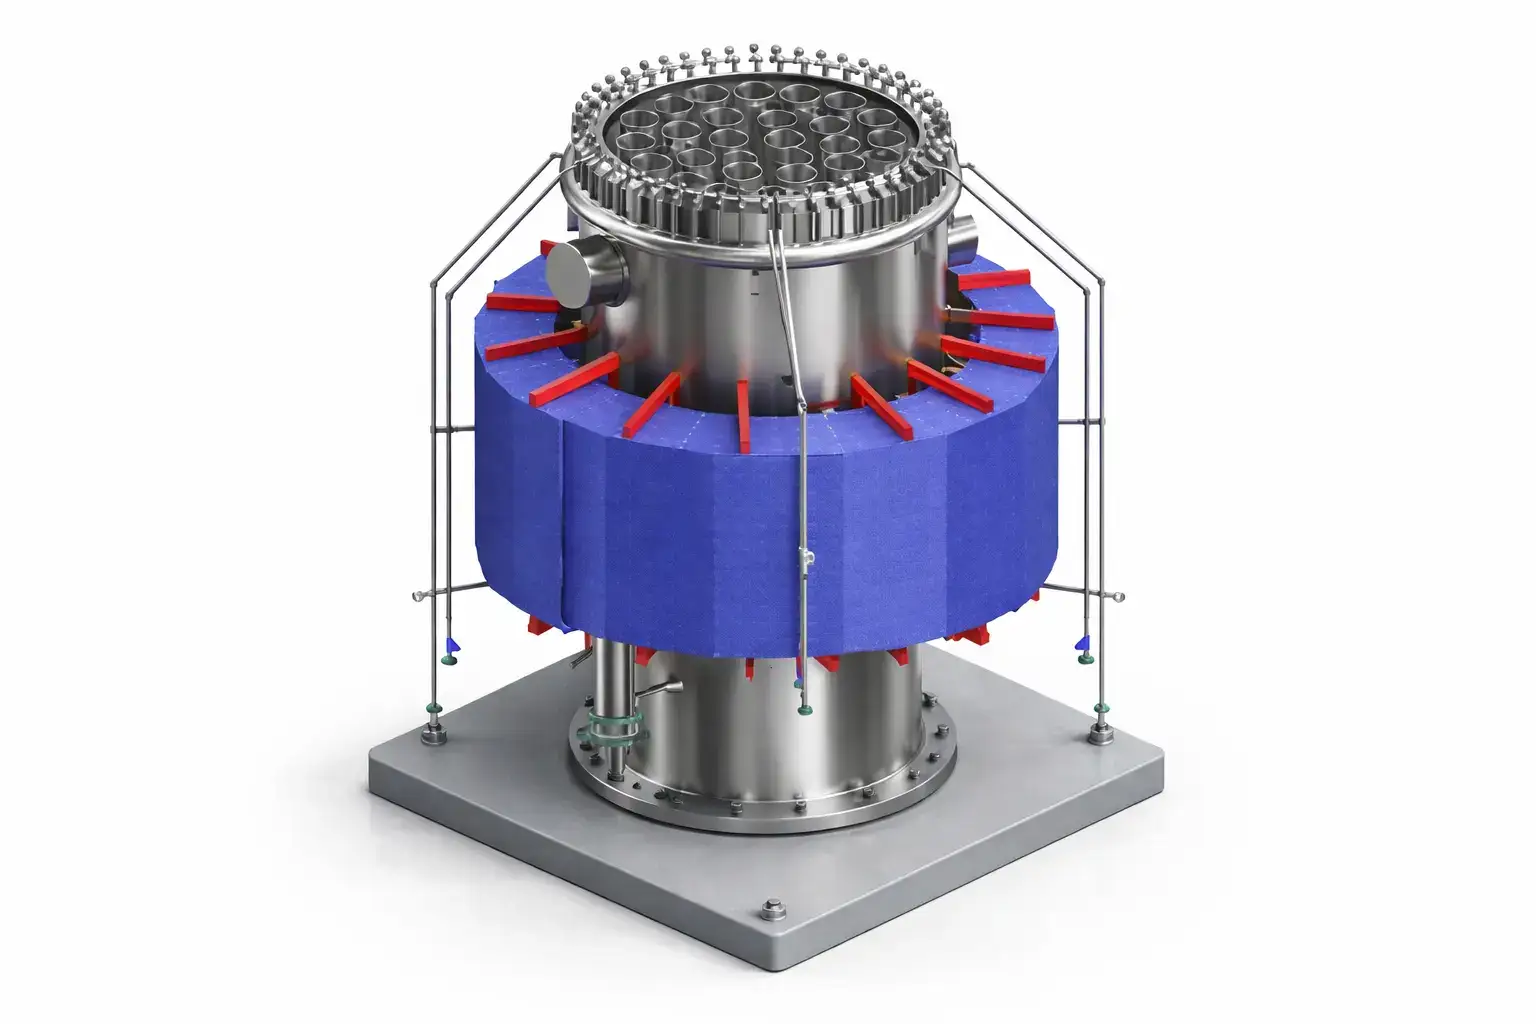
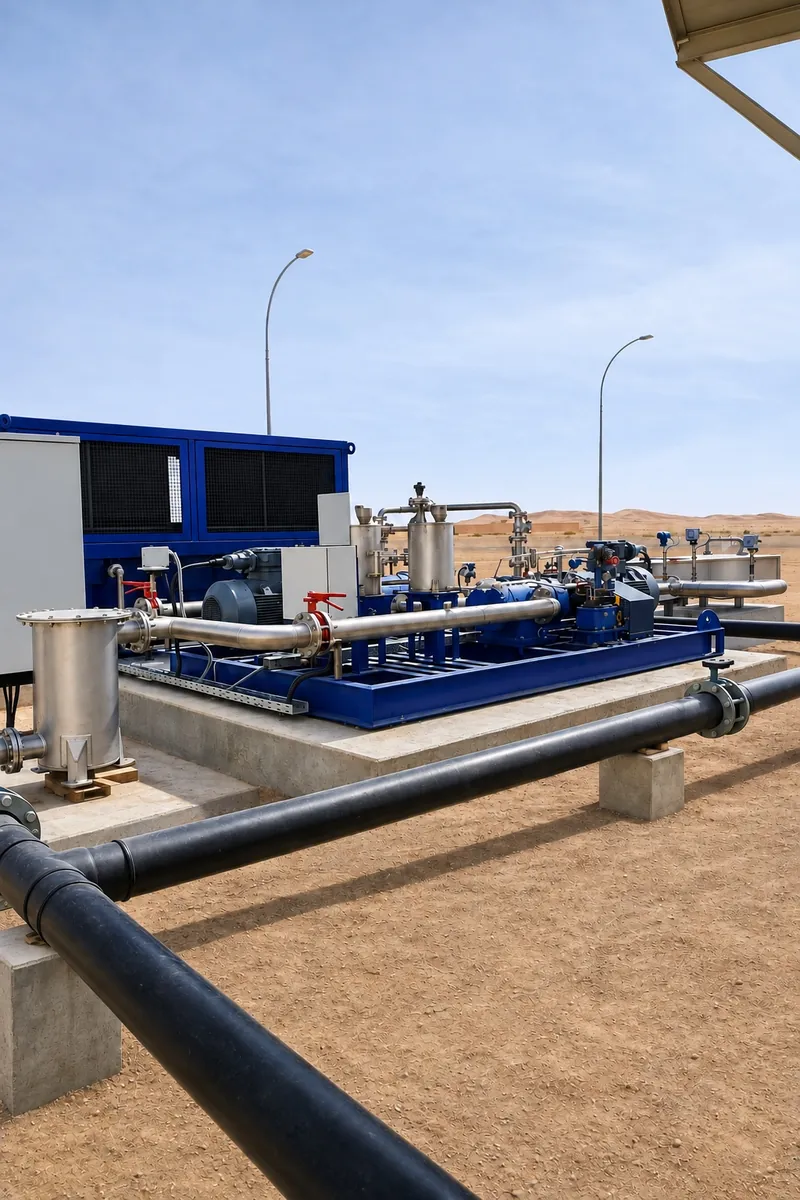
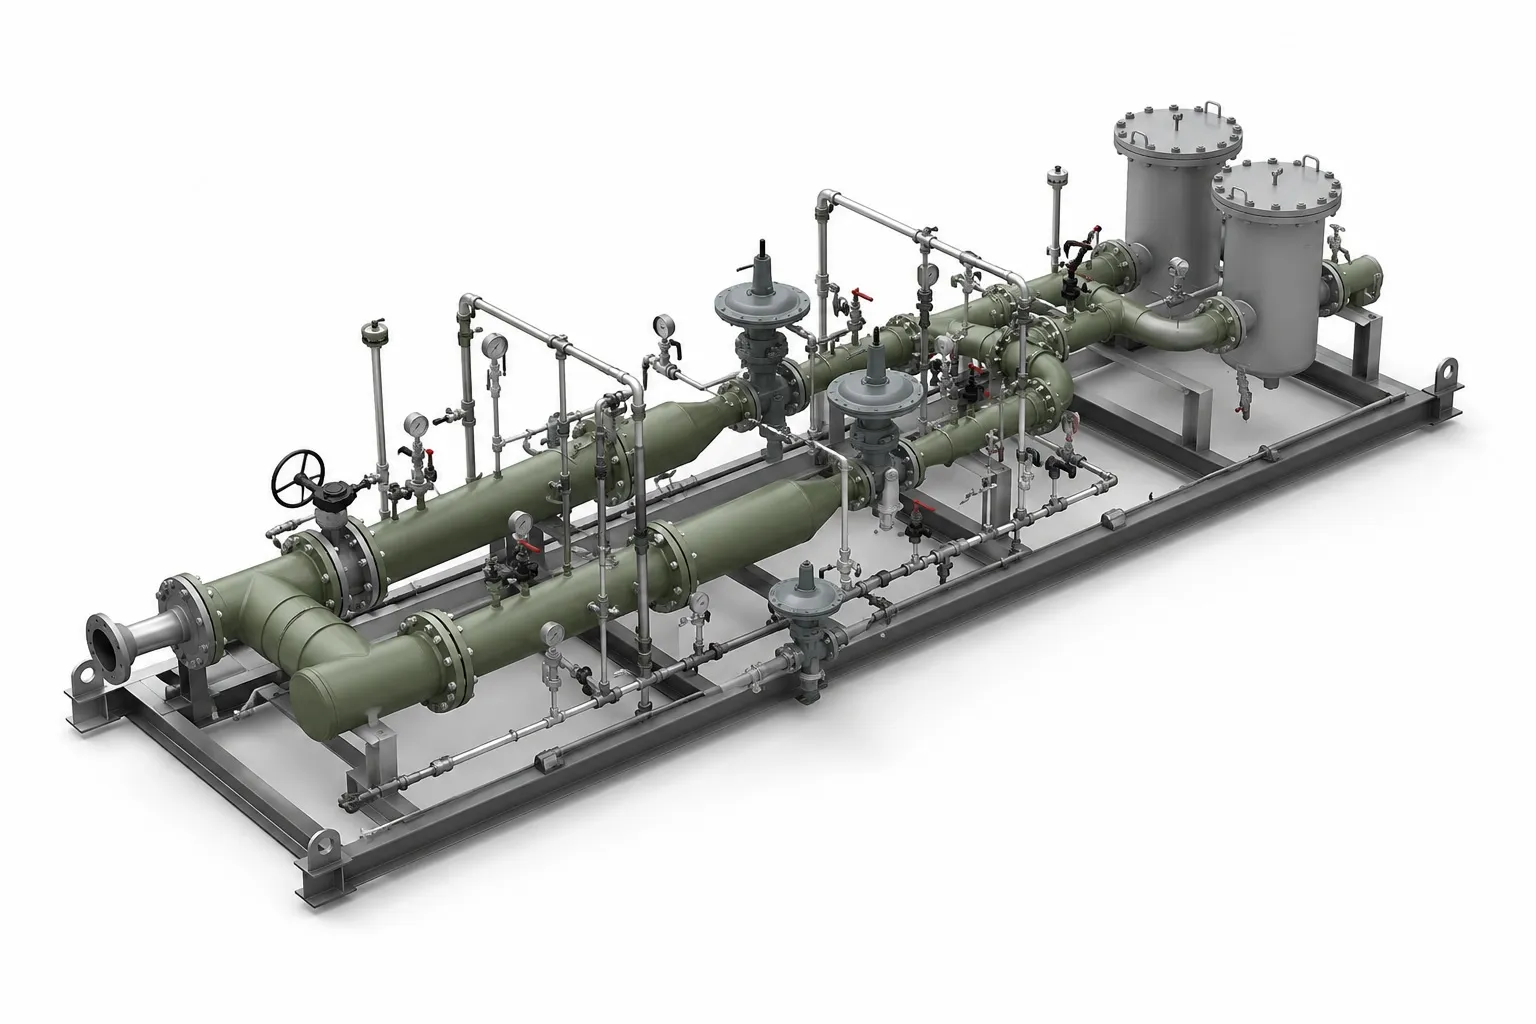
Handles purge-only to full emergency relief at 358 t/h with minimised purge gas consumption.
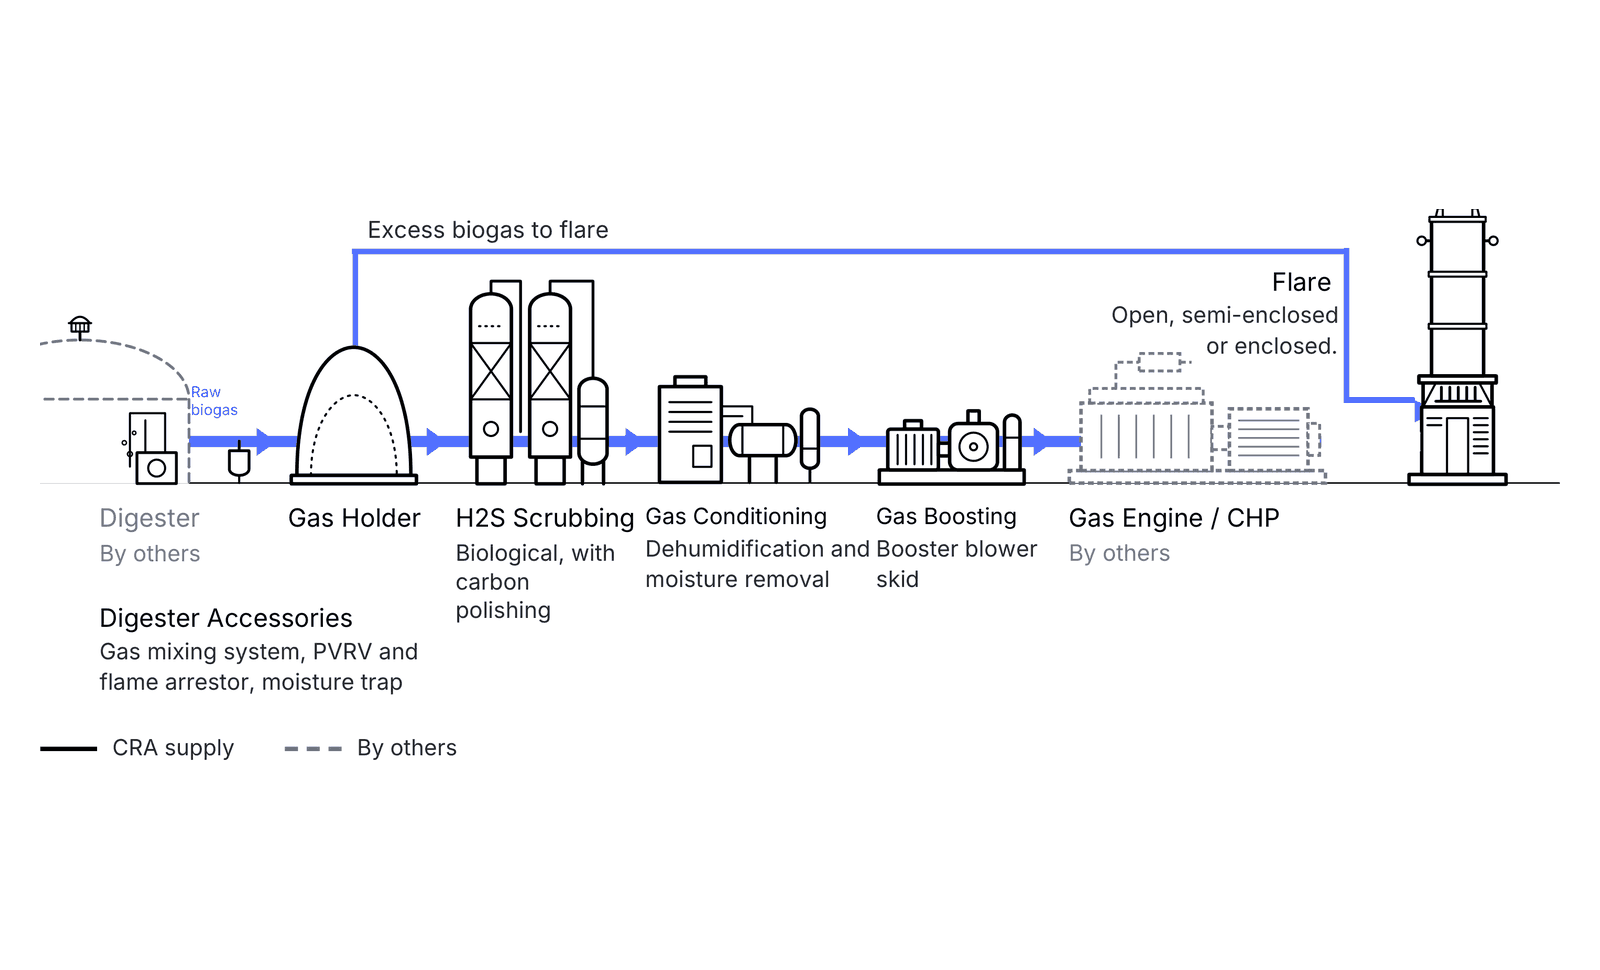
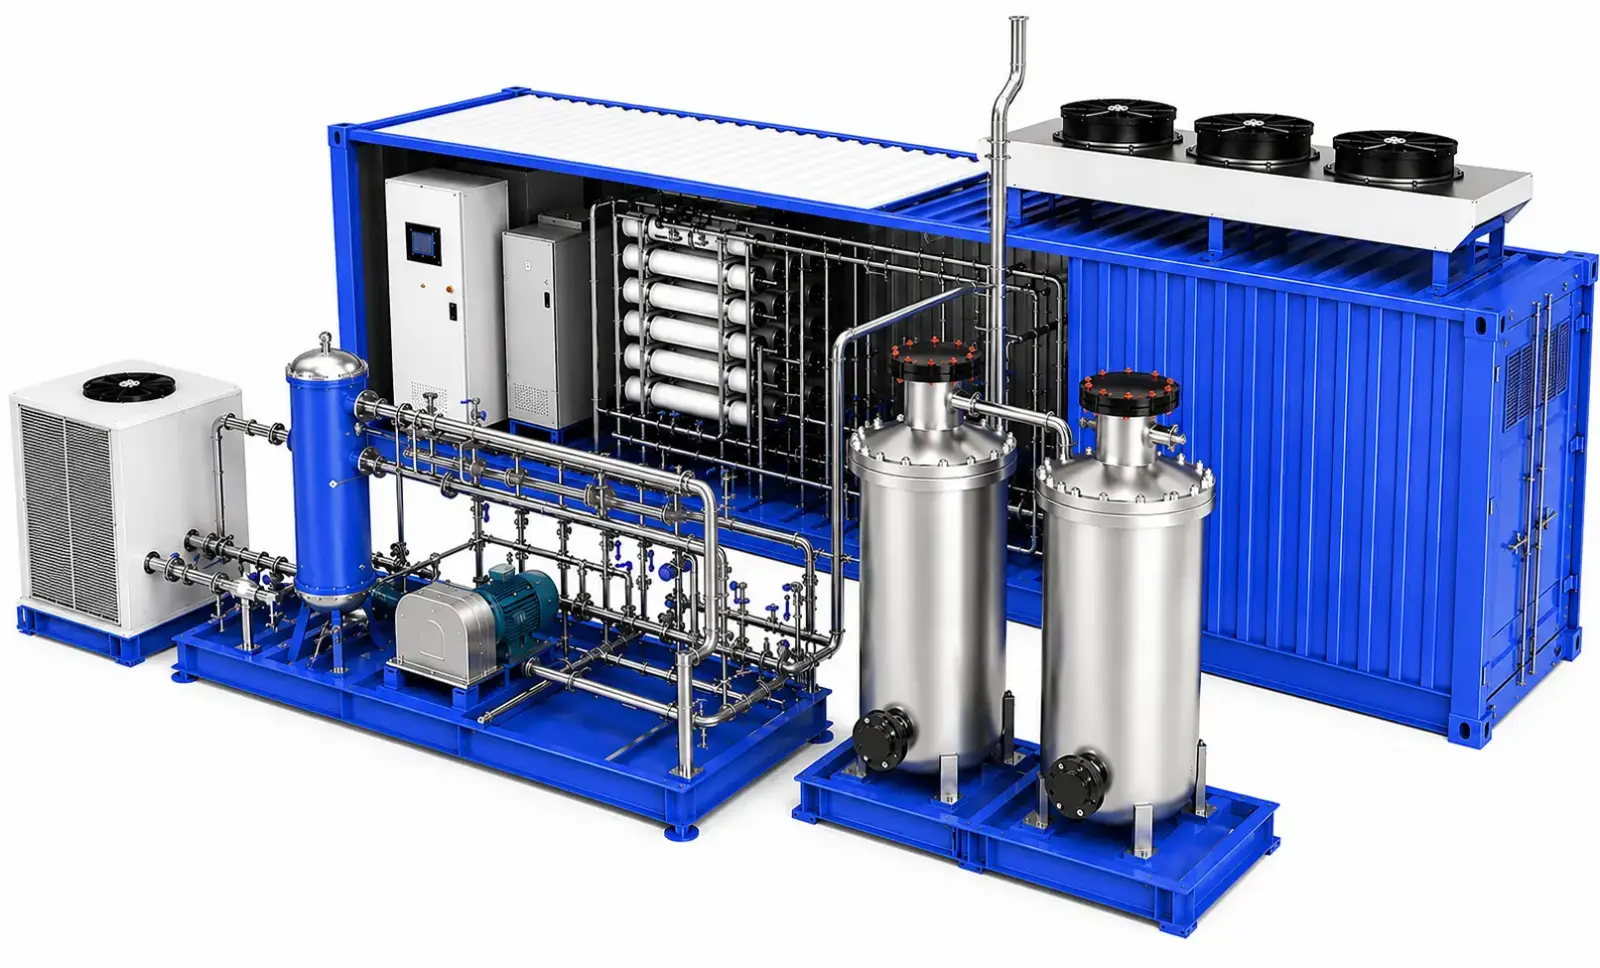
Two biological scrubbers designed in line with CE requirements, with outlet H₂S below 200 ppm, engineered for export deployment.
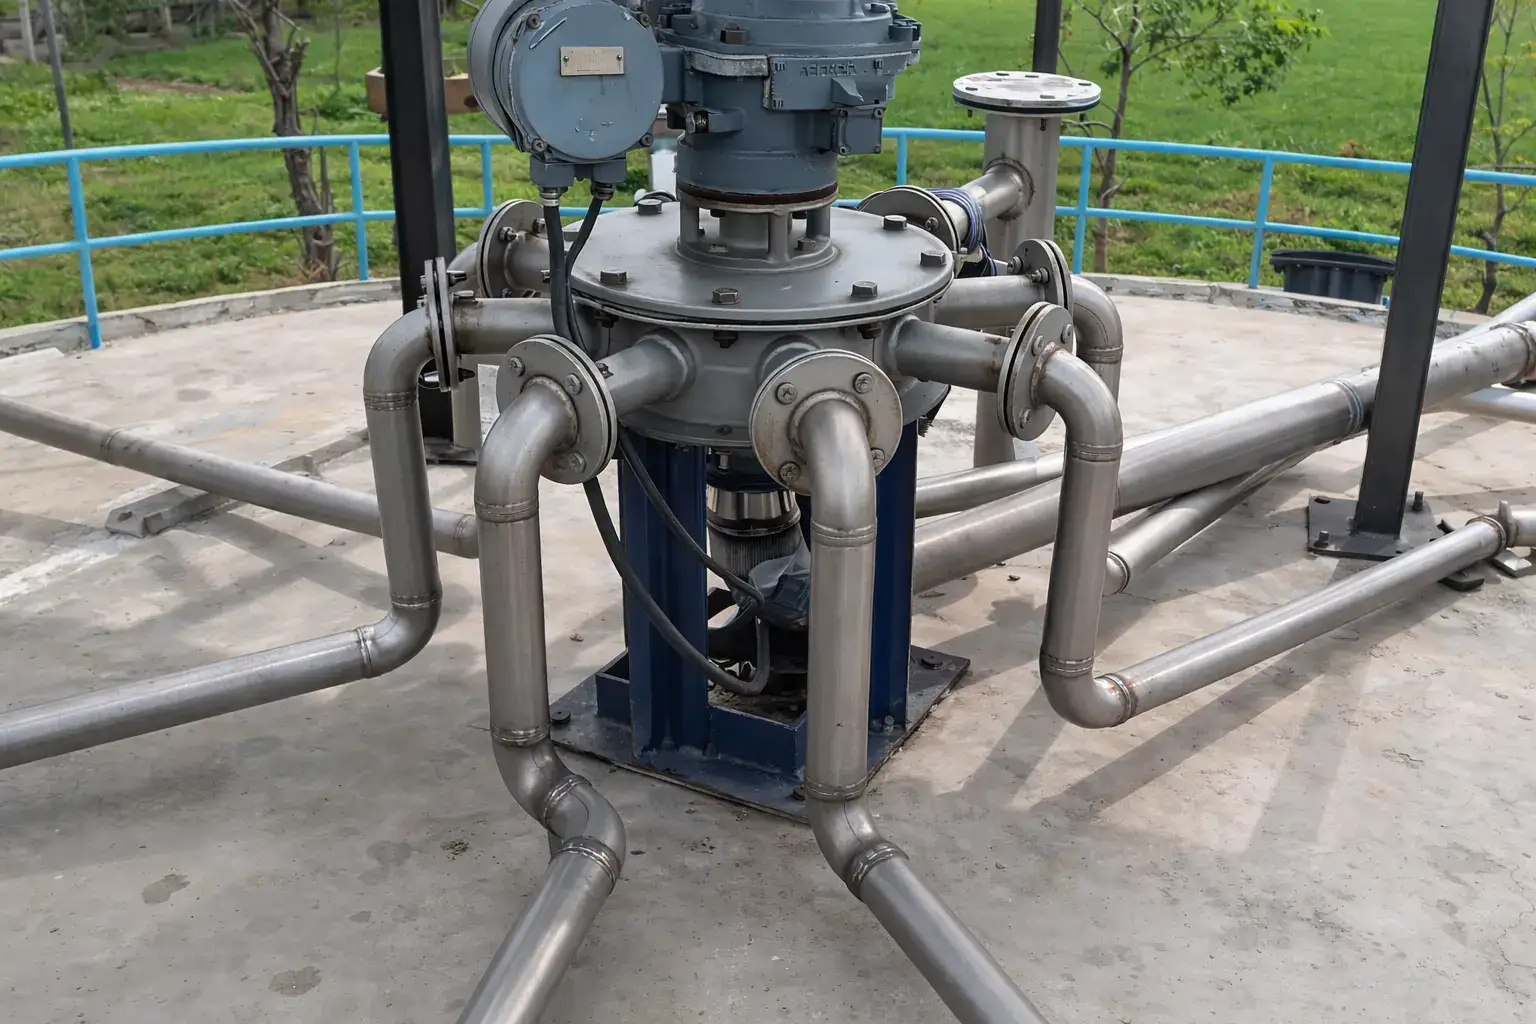
Continuous recirculation with automated gas distribution and no mechanical mixers inside the digesters.
Trusted by leading operators across 25+ countries

Gas Engineering Systems
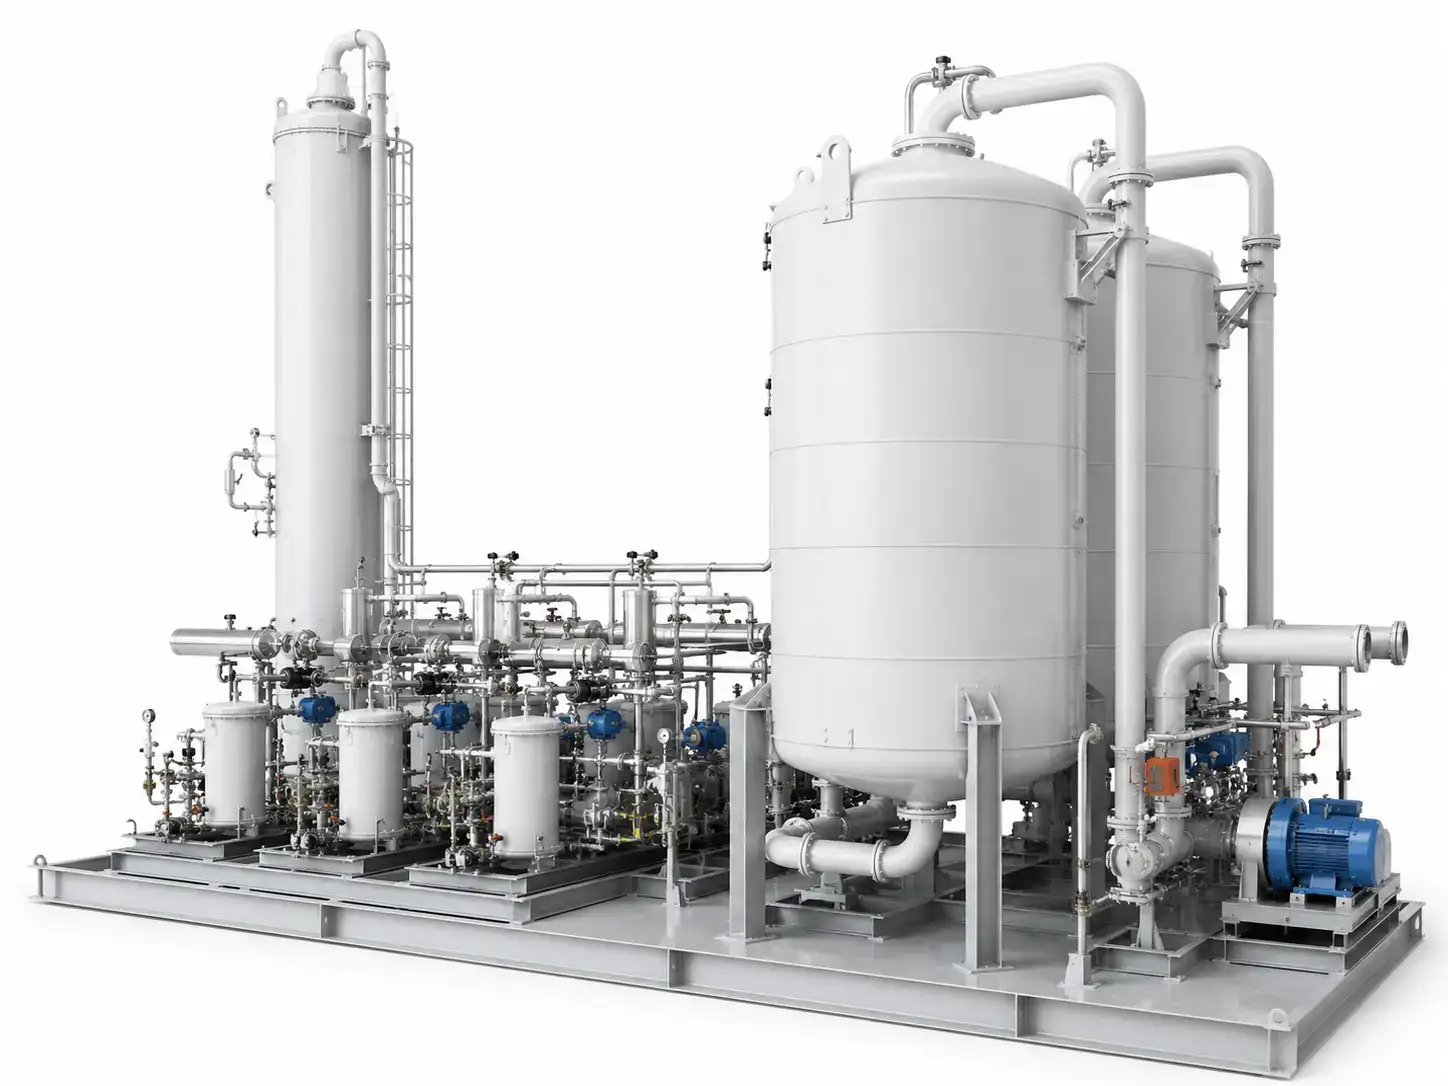
Custom-engineered and built in-house, our flaring, thermal oxidation, biogas, and gas processing systems are designed for safety, compliance, and uptime.
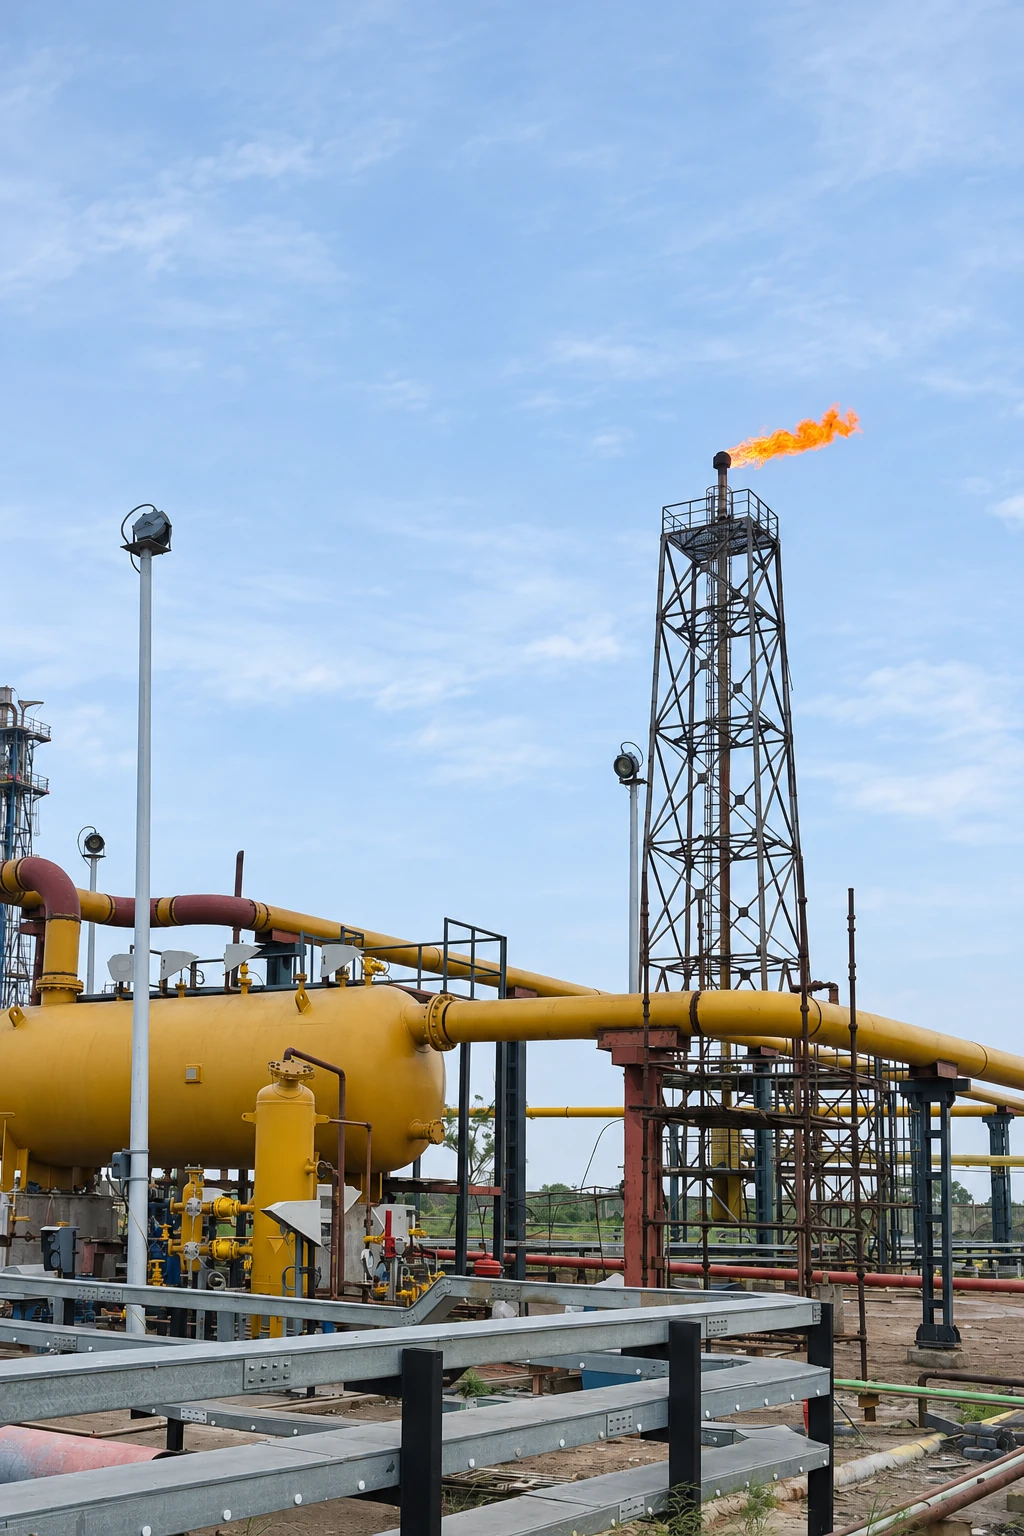
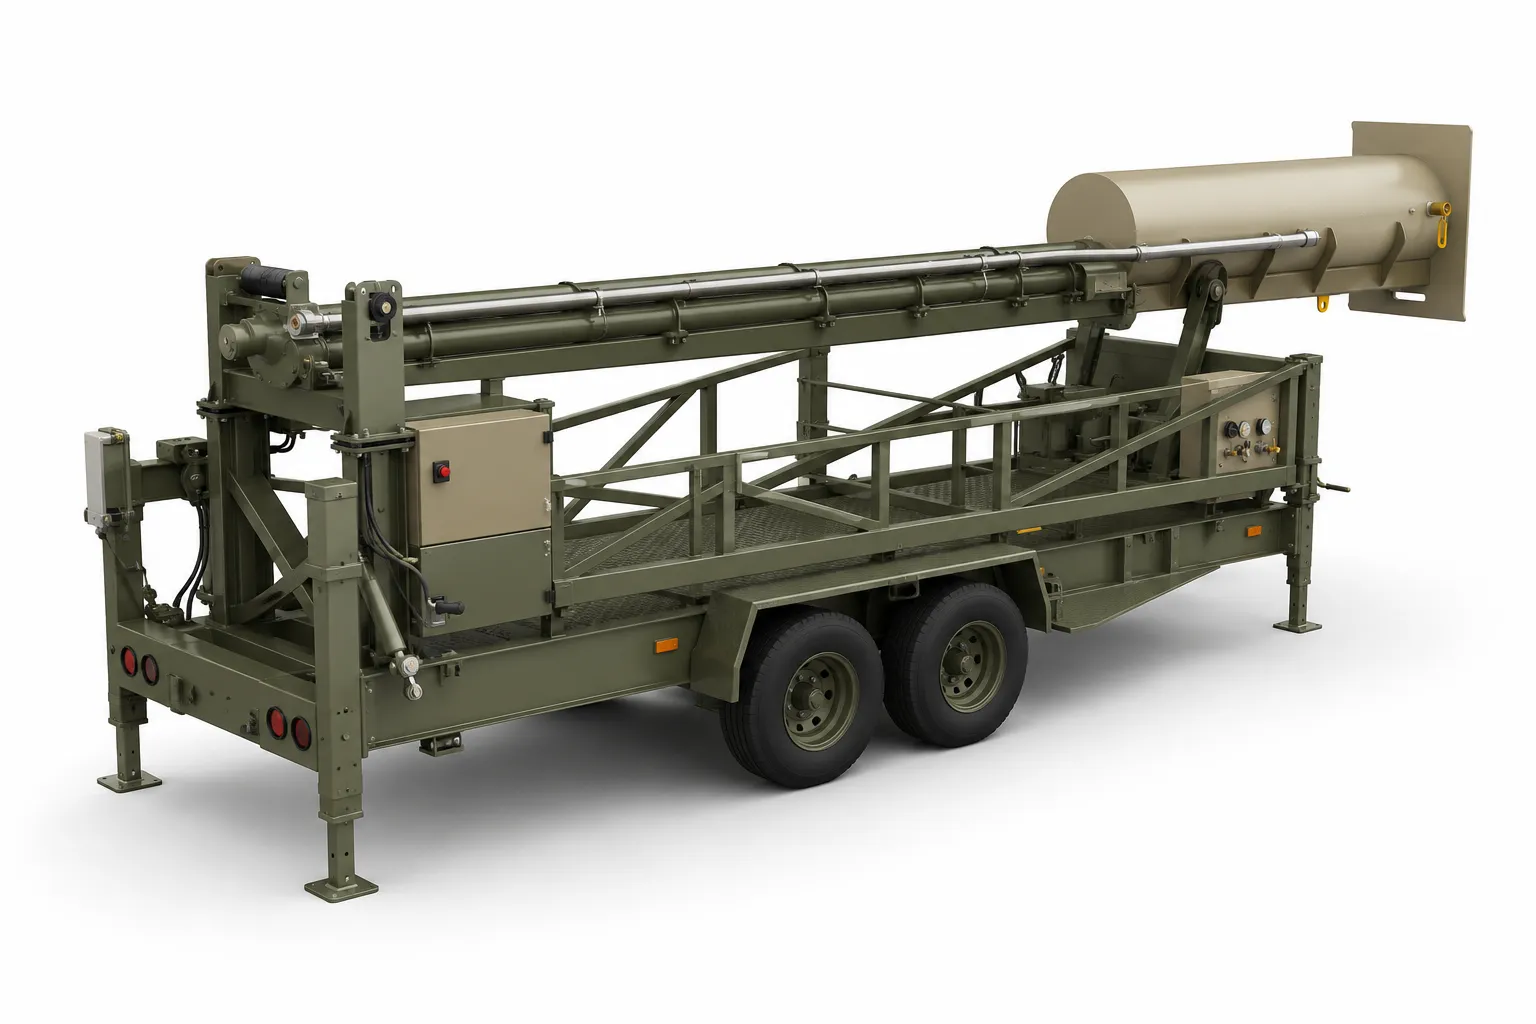
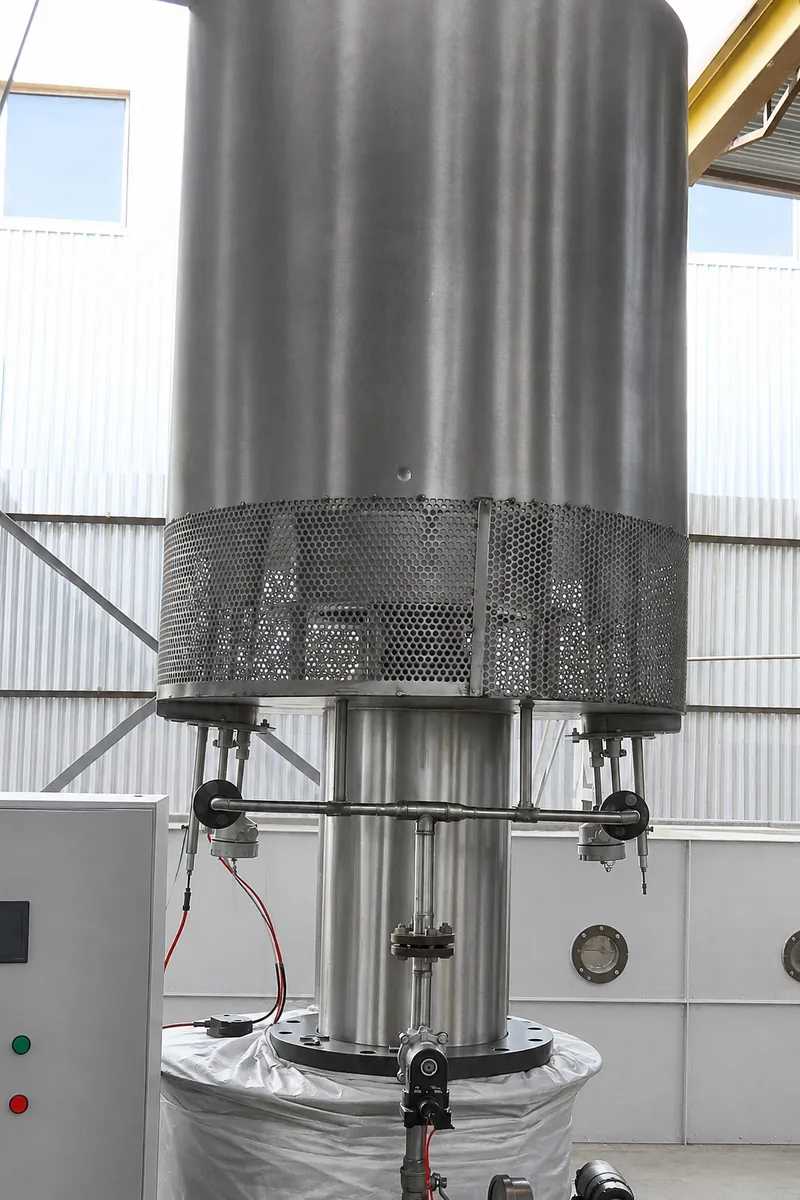
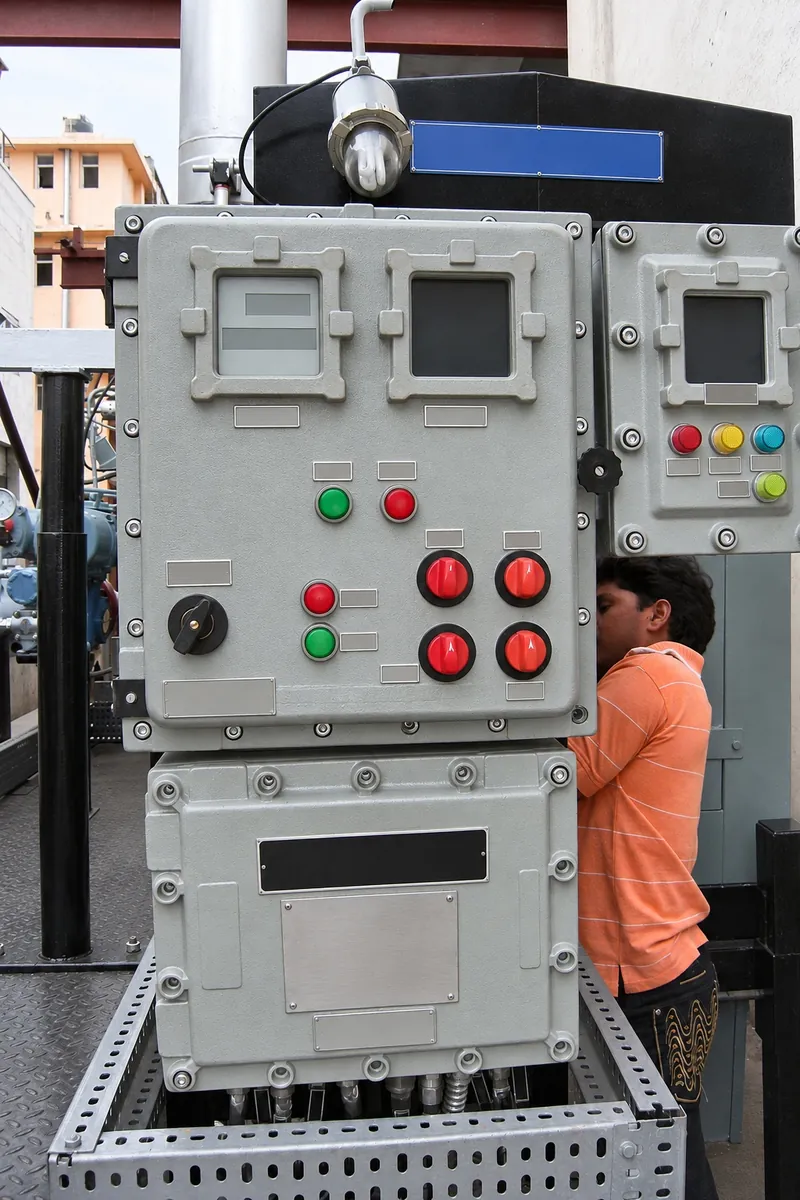
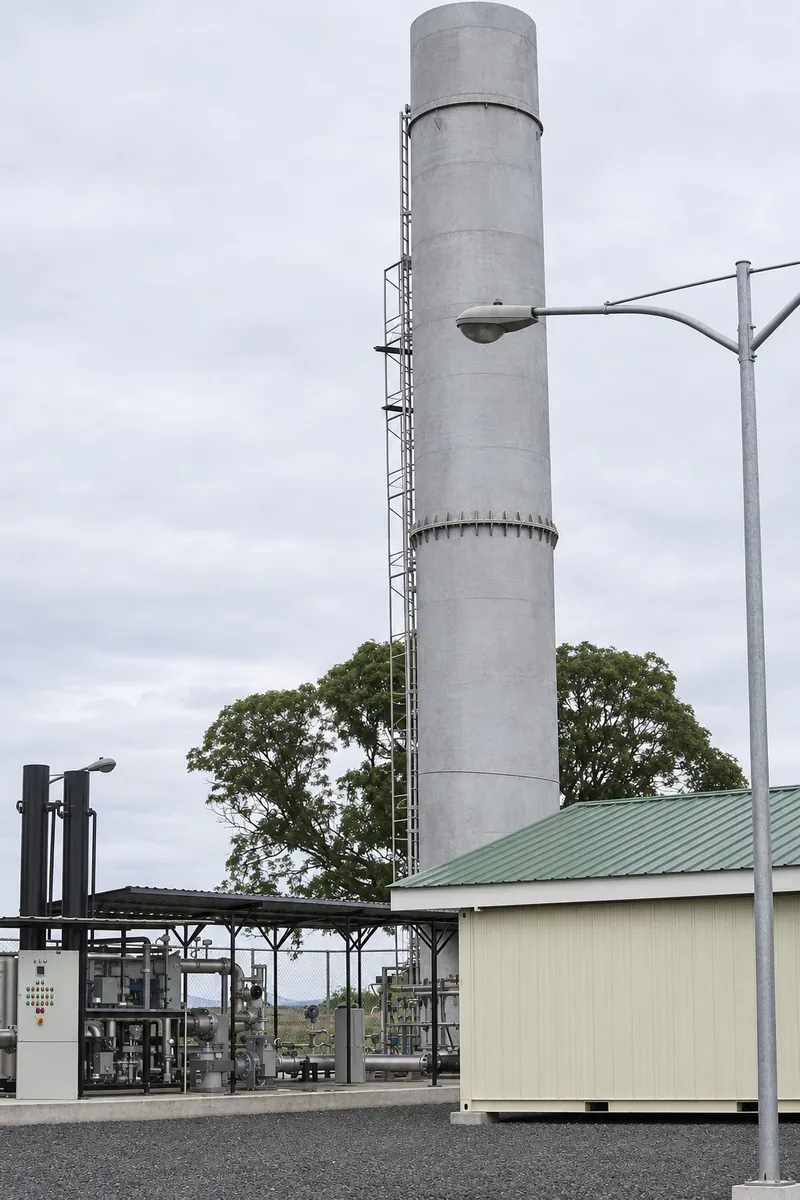
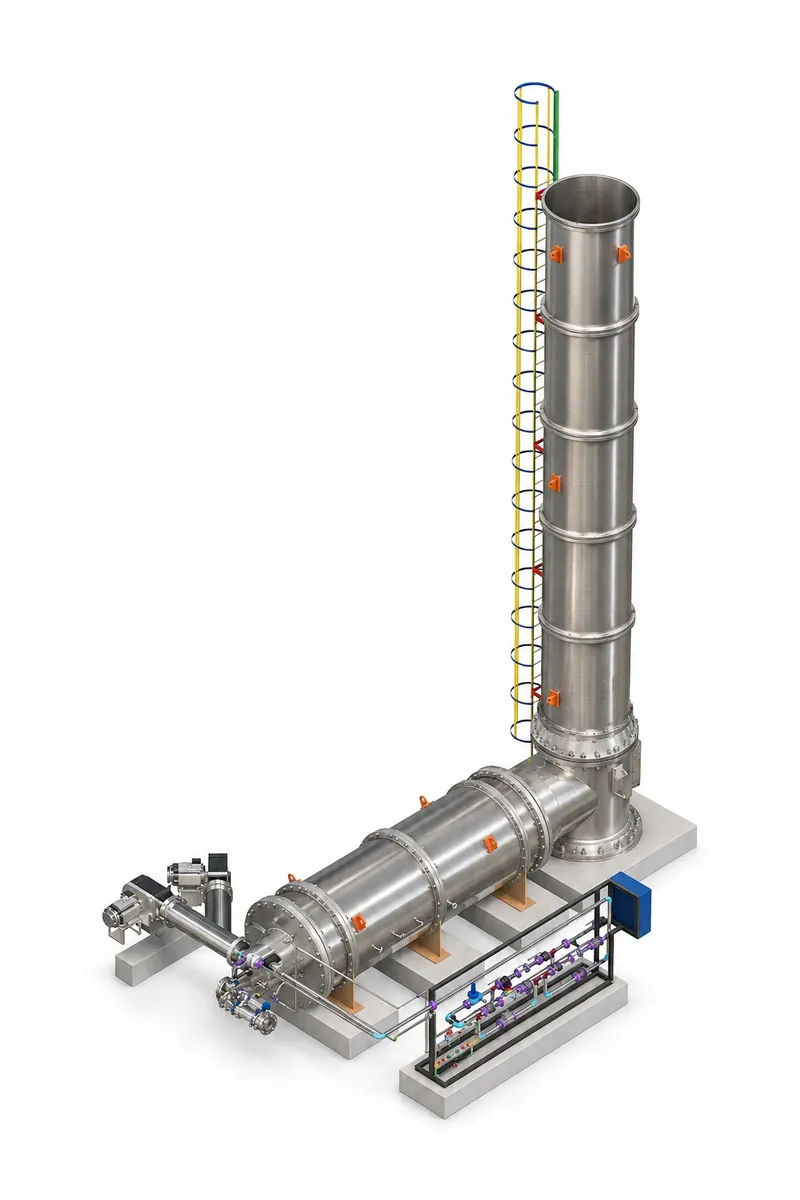
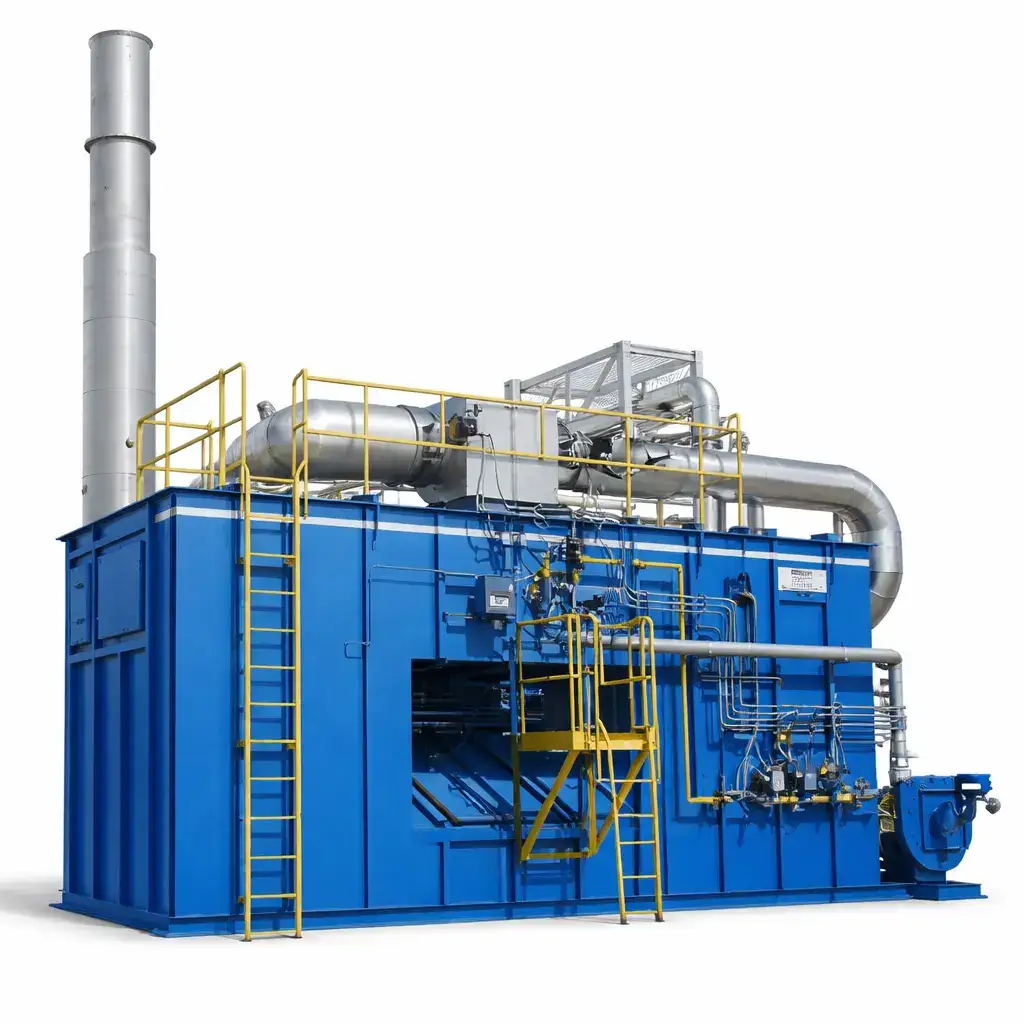
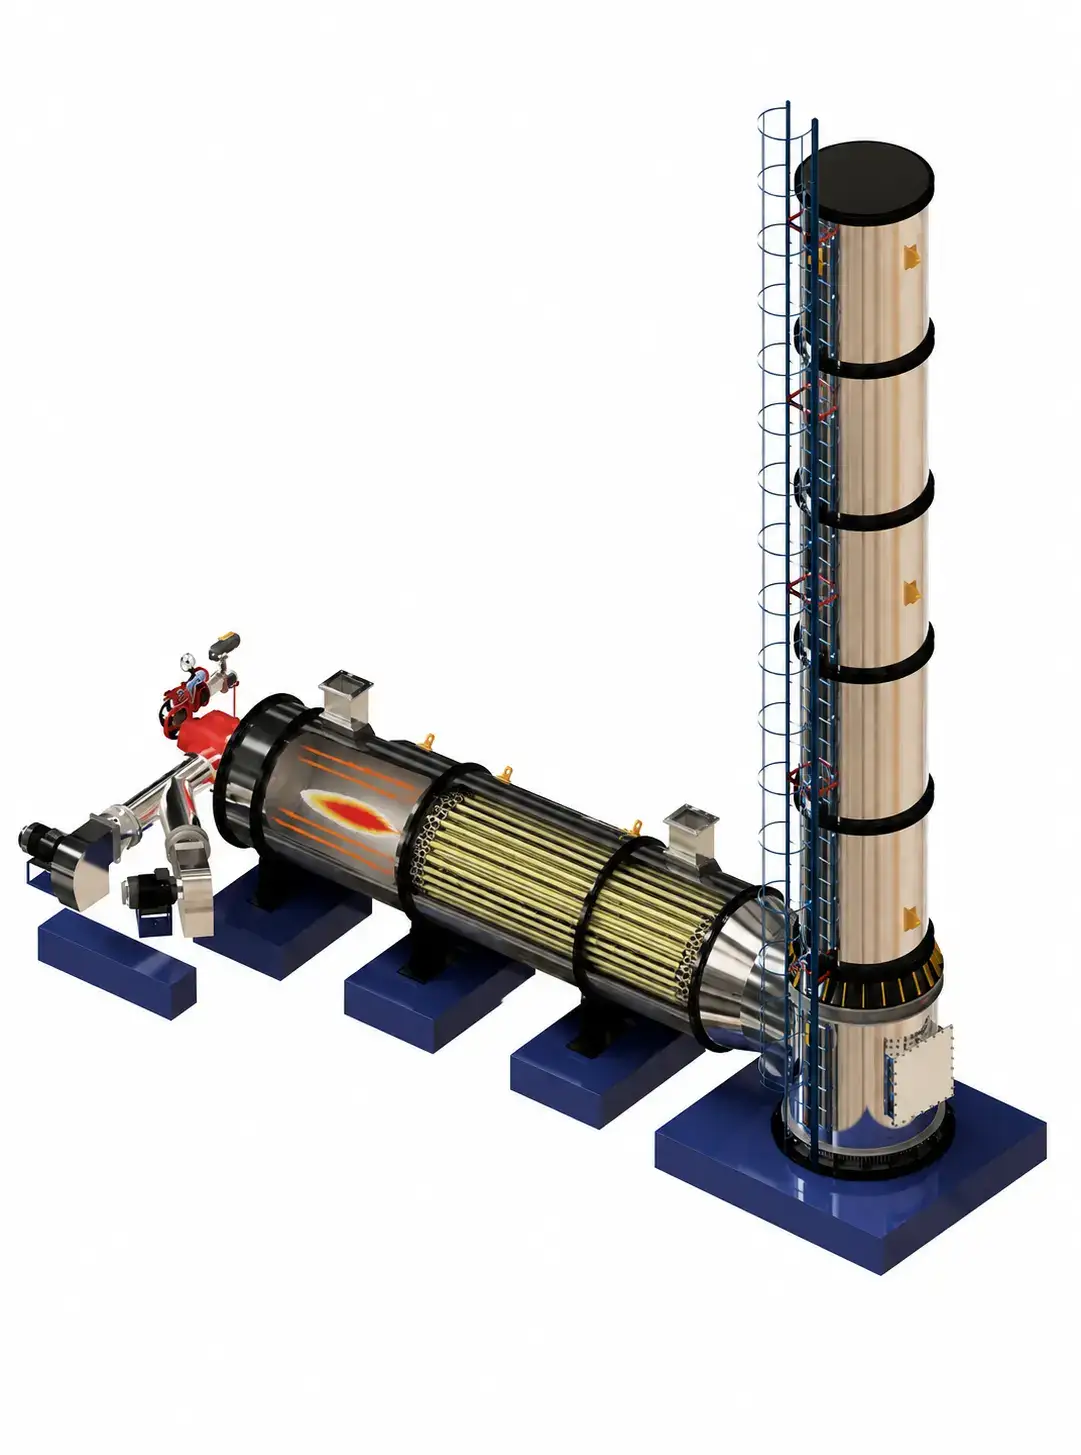
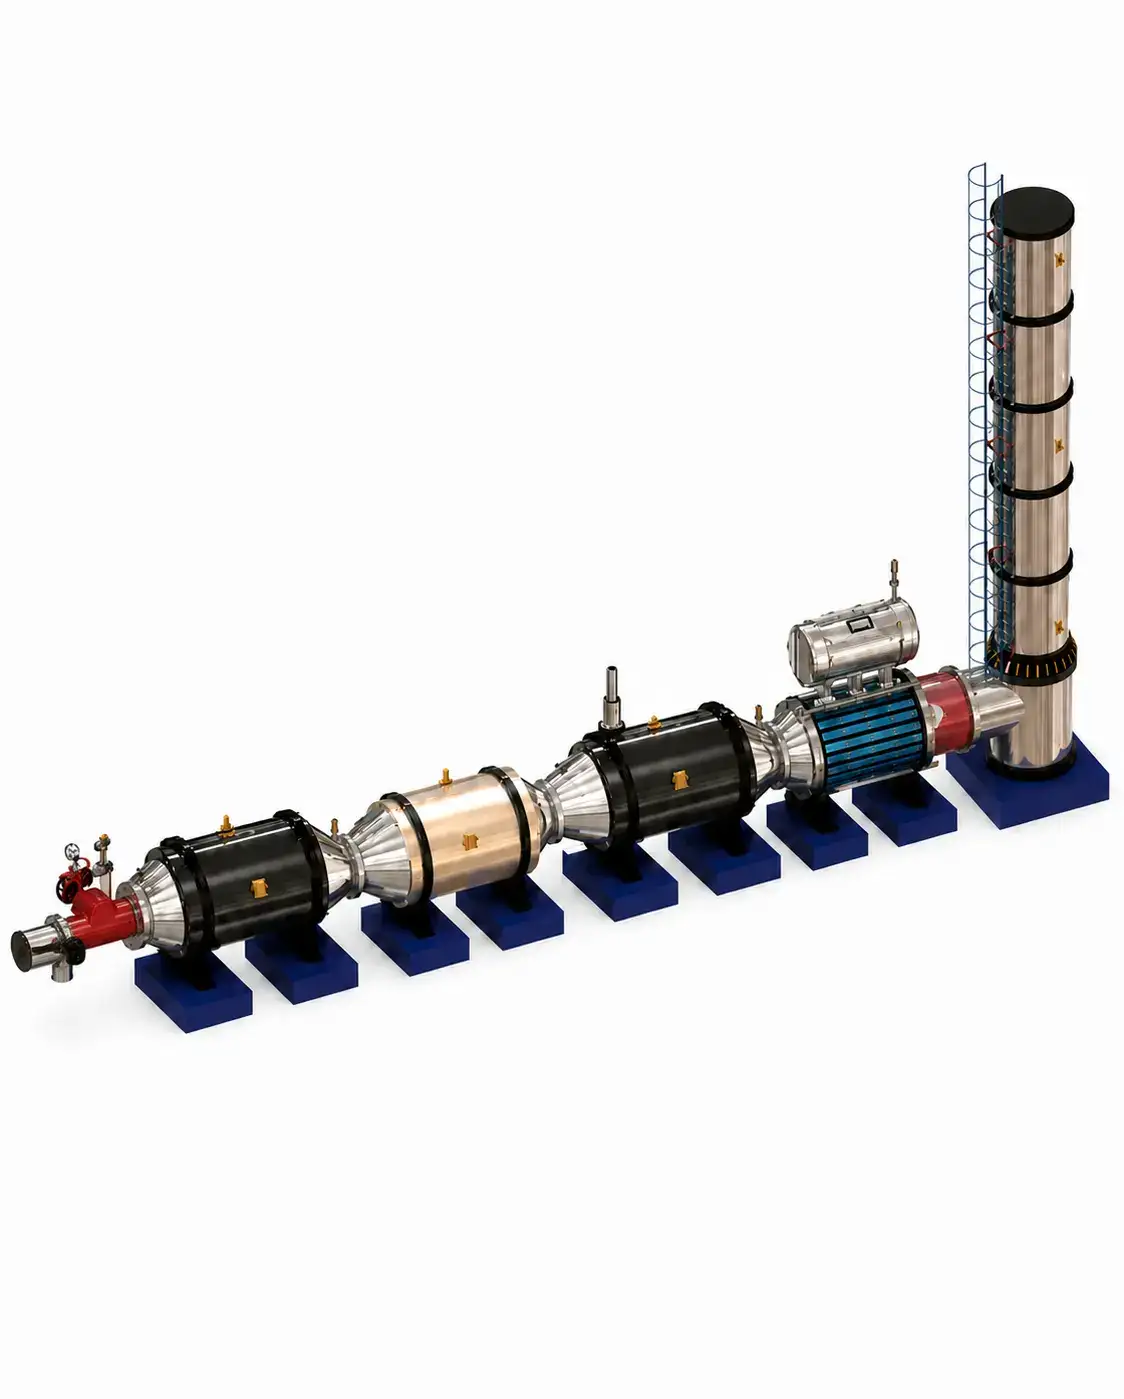
Selected industries
From hard problems to dependable systems


Services across the project lifecycle
Field services, retrofits, operations & maintenance and long‑term service agreements to keep your gas systems compliant, reliable and performing.
Delivered across continents
A track record across regions, climates, operating conditions, and regulatory standards

Installations
Countries including India, the United Kingdom, Singapore, and Canada
Years of custom engineered solutions for our clients



Custom engineered. Properly scoped.
Speak to an engineerFrequently Asked Questions
Get all the technical details and resources you need in one place.
What does CRA design and manufacture?
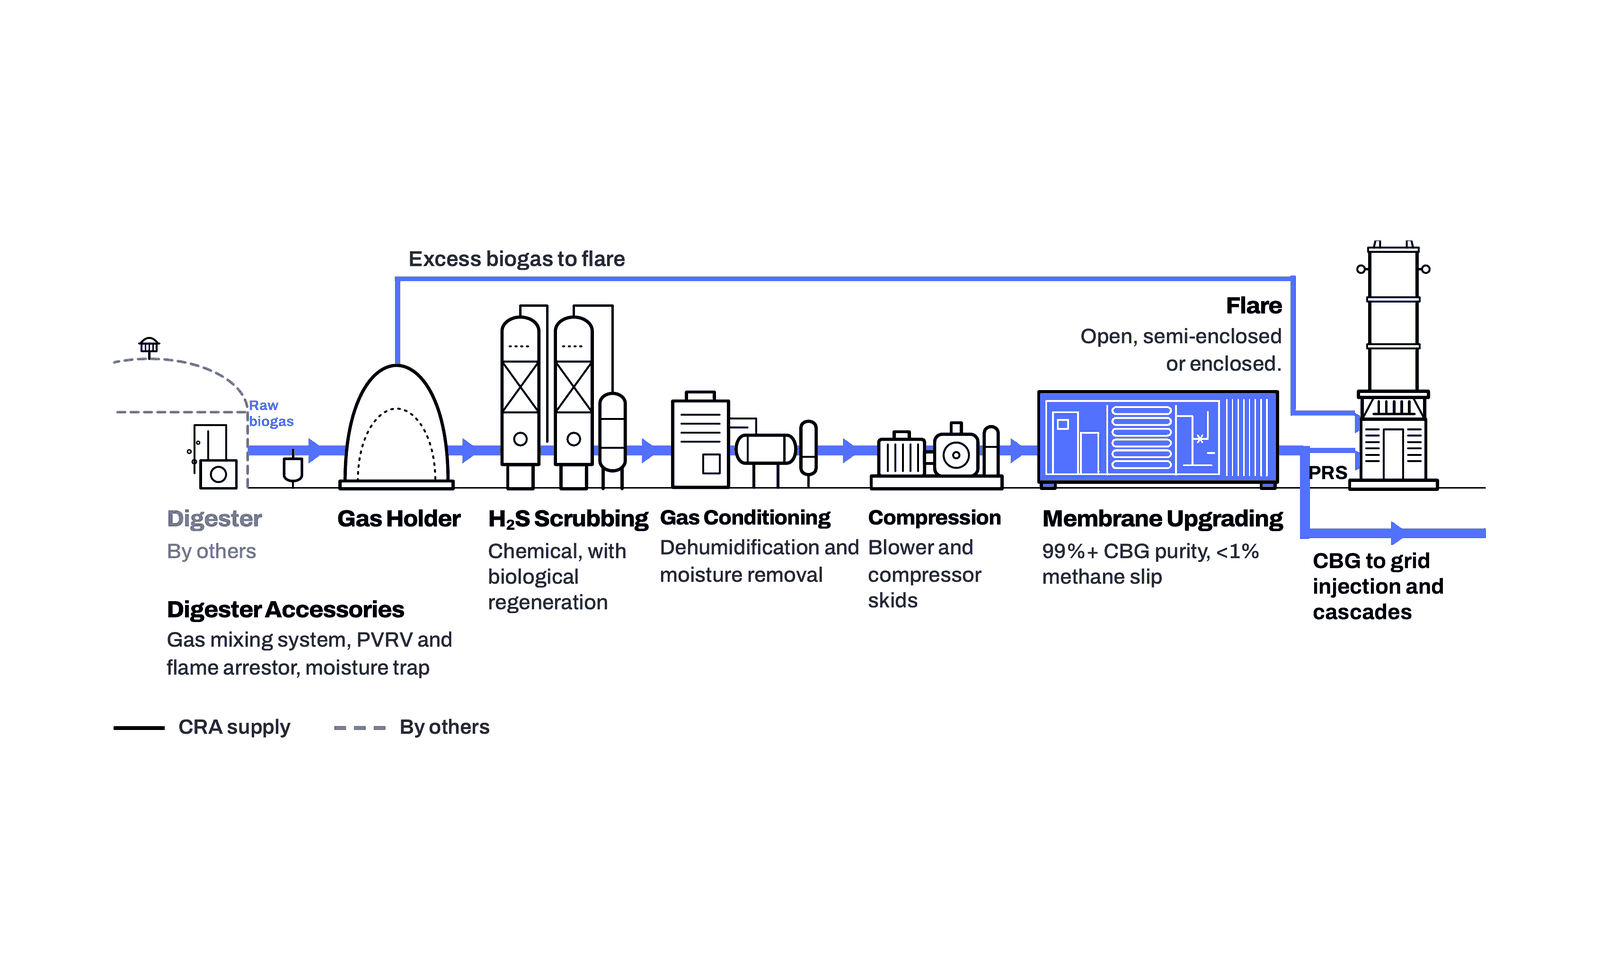
CRA designs and manufactures flares, thermal oxidisers including regenerative thermal oxidisers, biogas gas trains and CBG upgrading systems, H2S scrubbers, gas compression and processing skids, and defence containers. The flare range covers open elevated, enclosed ground, steam assisted, biogas and landfill gas flares, and CRA built the largest enclosed ground flare in India.
Mechanical, electrical and process design is done in-house at CRA's two factories in Noida, India, with its own fabrication and machining. CRA is an authorised packager and distributor for Ro-Flo rotary vane compressors and an Air Products membrane integration partner. Case studies cover these product lines.
Is CRA only in India, or does it operate internationally?
CRA operates internationally from its base in Noida, India. It has more than 800 flare, thermal oxidiser, gas processing and biogas installations in over 25 countries, most of them for repeat clients. Installations are in India, Southeast Asia, the Middle East, Africa, the UK, Australia, Canada and Latin America, including Ecuador and Colombia. CRA delivered its first export projects in 2010.
Every system is designed and built at CRA's two factories in Noida by a team of about 150 people, with mechanical, electrical and process design and fabrication in-house. The same engineering and quality process applies whatever the destination. Case studies cover projects in these regions.
Does CRA's equipment meet international standards like CE, API, and ISO?
CRA designs its equipment in line with the applicable requirements of API, CE/UKCA, IECEx and ATEX, and its quality management system is ISO 9001 certified through TÜV NORD, covering design, manufacturing and inspection. CRA's manufacturing facility is approved by ORDAQA and MSQAA for defence grade equipment production, and CRA is a registered vendor with PUB Singapore.
The same design standards and quality system apply across every product line and every destination market. A flare, thermal oxidiser or biogas system engineered in Noida is specified against the standards named in the client's enquiry for the jurisdiction where it will operate.