Biogas Processing Package: H2S Scrubbing, Dehumidification and Gas Boosting
Complete gas conditioning train transforming raw digester gas into clean, usable fuel for a city utility.
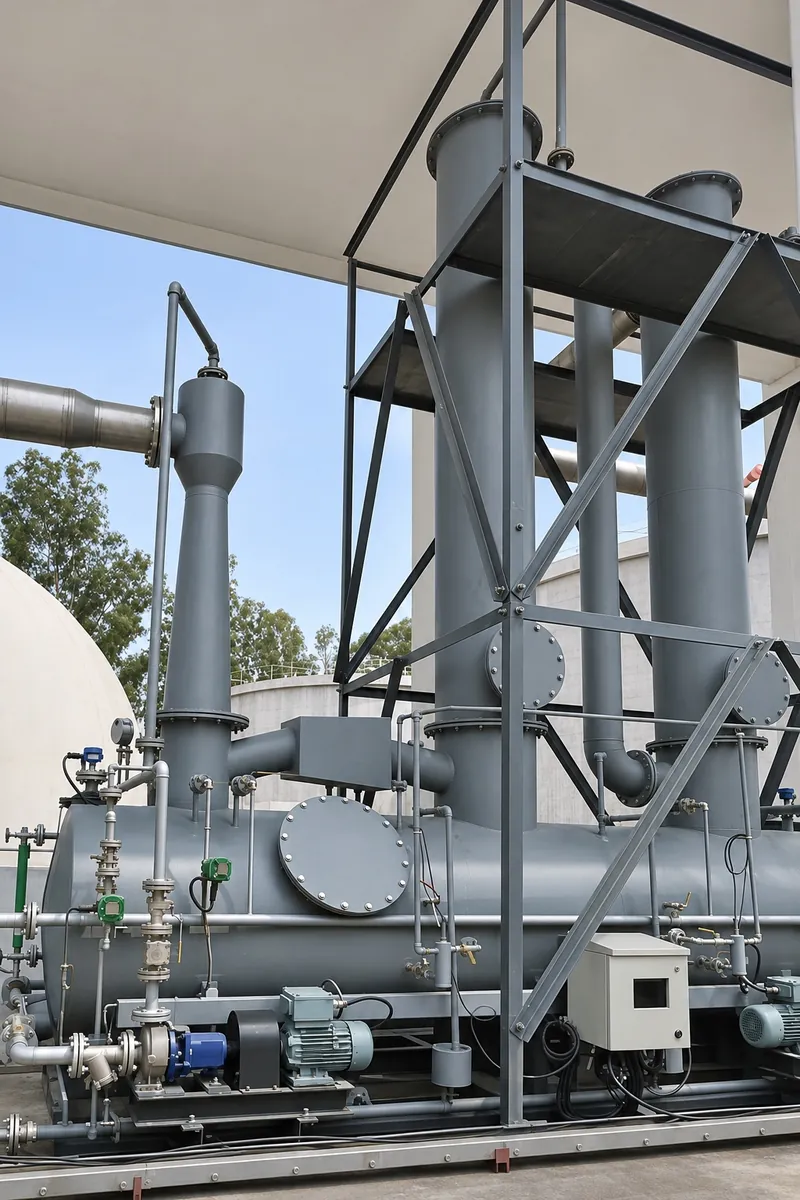
The project aimed to transform digester gas, a byproduct of anaerobic sludge digestion, into a clean, safe, and usable fuel source, while providing a route for excess gas disposal designed to meet emission norms. CRA engineered a fully integrated system comprising an H₂S Scrubber, Dehumidifier, Gas Booster, and Open Flare, supporting reliable gas quality management and operational safety for continuous plant operation. This package became a key milestone in Delhi Jal Board’s sustainability roadmap, supporting renewable energy generation and efficient biogas handling at one of the city’s major wastewater treatment facilities.
High H₂S, moisture, variable flow, and integration constraints
- High H₂S Content: Raw digester gas contained elevated levels of hydrogen sulphide, posing risks of corrosion, odour, and safety hazards.
- Moisture-Rich Gas: The saturated biogas led to condensation in pipelines and downstream equipment, reducing efficiency and damaging components.
- Variable Gas Flow and Pressure: Fluctuations in digester gas generation required a system capable of stable operation under changing flow and pressure conditions.
- Environmental Compliance: Meeting emission norms demanded smokeless and complete combustion during biogas flaring.
- Integration with Existing Infrastructure: The new system had to integrate with the plant operator’s process layout, control architecture, and operating schedule.
Comprehensive biogas treatment and control system
CRA engineered and delivered a comprehensive biogas treatment and control system, built for reliability, efficiency, and minimal maintenance in demanding wastewater plant environments.
Biogas Scrubbing System
- Capacity: 1200 Nm³/hr
- Purpose: Removal of H₂S and trace impurities using a packed-bed chemical scrubbing process.
- Design Features:
- Multi-stage scrubbing tower for enhanced gas-liquid contact efficiency.
- Corrosion-resistant construction for long service life.
- Automatic dosing to maintain consistent scrubbing performance.
- Outcome: Achieved outlet H₂S levels of <100 ppm, protecting downstream components and supporting safe combustion.
Biogas Dehumidifier (Drier)
- Capacity: 1200 Nm³/hr
- Purpose: Moisture removal from scrubbed gas prior to compression and utilisation.
- Design Features:
- Refrigeration-based cooling to lower the dew point.
- Automatic condensate drainage and real-time temperature control.
- Integrated skid with corrosion-resistant piping and sensors.
- Outcome: Delivered consistently dry biogas, preventing corrosion, enhancing burner efficiency, and supporting stable flare operation.
Gas Booster System
- Purpose: Pressure boosting for biogas transfer to flare and optional energy recovery units.
- Design Features:
- Positive displacement blower with a flameproof motor.
- Safety interlocks for over pressure and reverse flow protection.
- Flexible coupling and vibration isolation for low-noise operation.
- Outcome: Maintained steady gas delivery pressure for consistent combustion and safe gas management.
Open Flare System
- Capacity: 450 Nm³/hr
- Purpose: Safe and complete combustion of surplus or unutilised biogas.
- Design Features:
- Pilot-assisted ignition with flame arrestors and flame detection sensors.
- Optimised air-fuel mixing for smokeless, high-efficiency flaring.
- Heavy-duty construction suitable for outdoor, continuous operation.
- Outcome: Achieved stable, smokeless flaring of excess gas, supporting environmental compliance and operational safety.
Engineering, fabrication, and assembly
CRA executed the engineering, fabrication, and assembly entirely in-house, supporting full control over quality and performance. The modular skid-mounted systems allowed quick installation and integration into the plant’s existing gas handling network.
Comprehensive commissioning and performance validation were carried out on-site, including flare ignition tests, gas quality verification, and automation checks. Operator training sessions were held at handover.
Enhanced Biogas Quality, Reliability, Sustainability
- Enhanced Biogas Quality: Effective Chemical H₂S Scrubber and moisture removal enabled reliable utilisation and safe flaring.
- Improved Safety and Compliance: Automated ignition, pressure control, and emissions management supported safe operation aligned with CPCB norms and oil and gas industry standards.
- Operational Reliability: Modular design with automated monitoring reduced manual intervention and downtime.
- Sustainability Boost: Enabled energy-efficient gas management at Delhi Jal Board’s wastewater treatment facility, supporting its renewable energy goals.
- Scalable Solution: The success of this system established a replicable model for biogas recovery and processing in municipal utilities across India.
Related Case Studies
See how we turn hard problems into high-performance infrastructure.