LFG Flare & Extraction System at Ghazipur Dumpsite, Delhi
Enclosed flare tower and extraction system handling 600 Nm3/h of landfill gas at DRE at or above 98%, designed to CPCB stack limits.
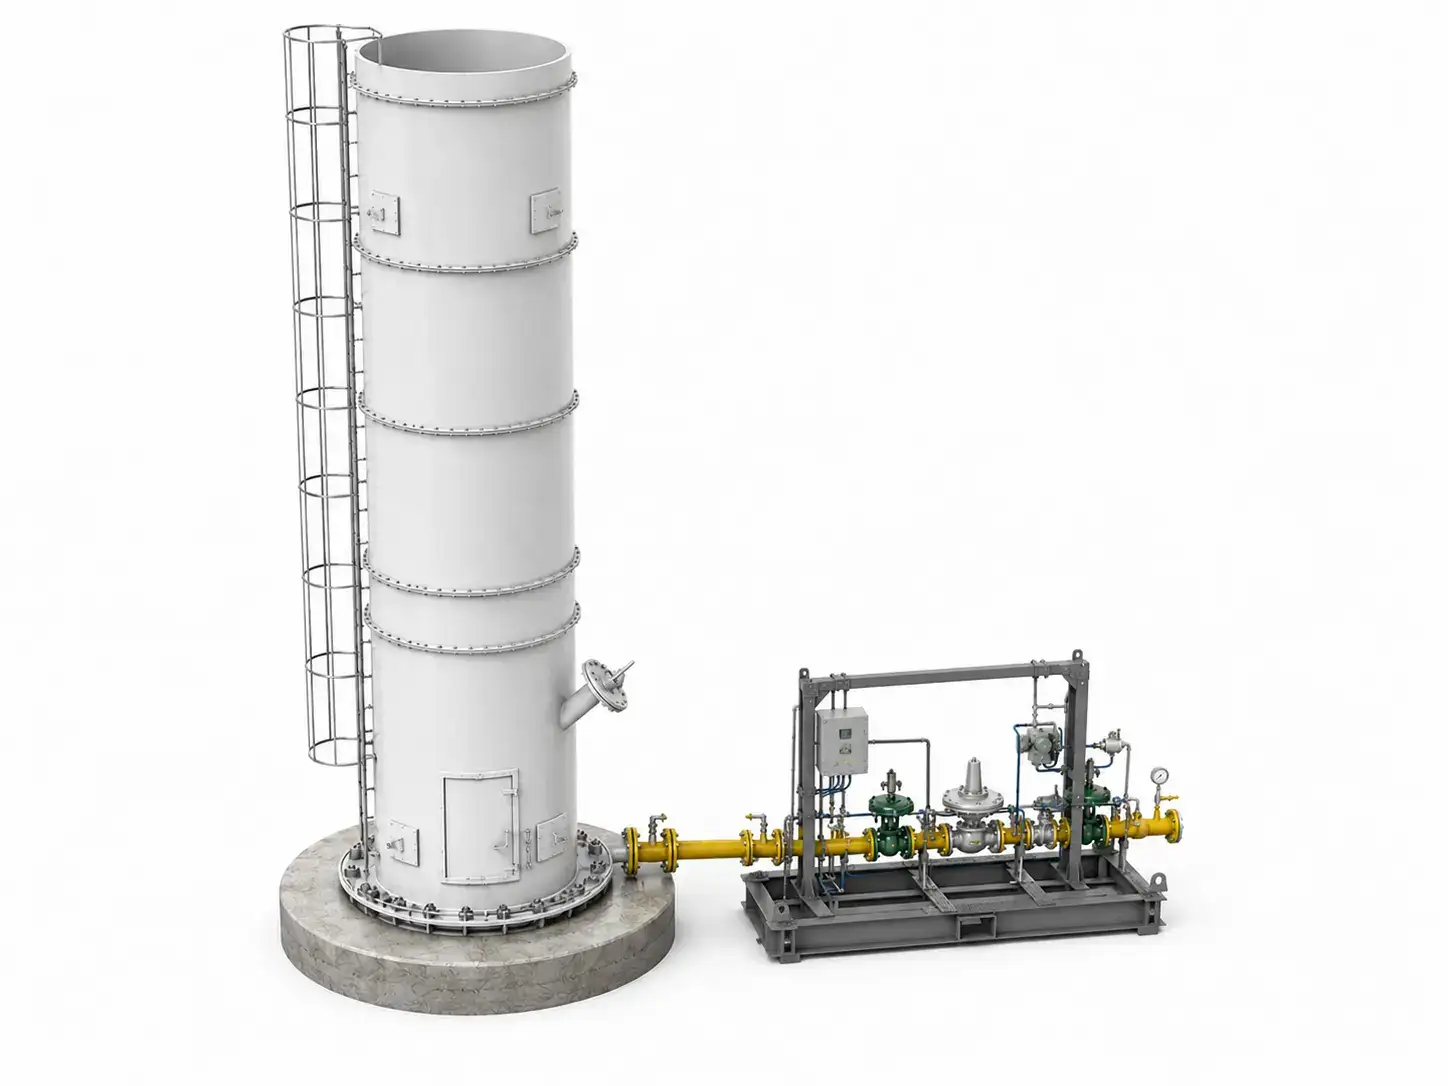
CRA executed the full scope of design, manufacture, installation and commissioning of an enclosed landfill gas flare system at the Ghazipur dumping ground in New Delhi, a GAIL funded landfill closure project. The system handles up to 600 Nm3/h of LFG at a DRE at or above 98%, designed to meet CPCB stack emission limits for CO, NOx and TOC.
Managing high volume landfill gas at a GAIL funded closure site in Delhi
GAIL funded the closure of the Ghazipur dumping ground in New Delhi and required a landfill gas flare and extraction system capable of handling variable gas composition at scale, while meeting CPCB stack emission limits for CO, NOₓ and TOC.
- Handling up to 600 Nm³/h of landfill gas of variable methane content
- Meeting CPCB stack emission limits for CO, NOₓ and TOC
- Reliable extraction of gas from the dumpsite ahead of combustion
- Delivering the full scope from design through commissioning on a government funded project
An integrated flare tower, gas train and extraction system
CRA executed the complete scope of design, manufacture, installation and commissioning for the Ghazipur landfill gas flare and extraction system.
Core system delivered
- Enclosed flare tower
- Skid mounted gas train with anti flashback burners
- Automated control panel with data logging
- Twin lobe extraction blower for landfill gas recovery
DRE at or above 98%, designed to CPCB limits
- System handles up to 600 Nm³/h of landfill gas at DRE ≥ 98%
- Designed to meet CPCB stack emission limits for CO, NOₓ and TOC
- Commissioned, with satisfactory performance confirmed by the contractor
- Anti flashback burners and PLC based controls supporting safe unattended operation
Delivering high capacity landfill gas management for a government funded closure
The Ghazipur project shows CRA’s capability to deliver a complete enclosed ground flare and extraction system for a large scale, government funded landfill closure. The combination of a purpose built flare tower, automated controls and a dedicated extraction blower gave GAIL and its contractor a system designed to CPCB limits at high gas volumes.
Related Case Studies
See how we turn hard problems into high-performance infrastructure.