Thermal Oxidizers for Sulphur Recovery Units
Thermal oxidisers that destroy the reduced sulphur compounds left in sulphur recovery unit tail gas.


Final destruction of sulphur in SRU tail gas
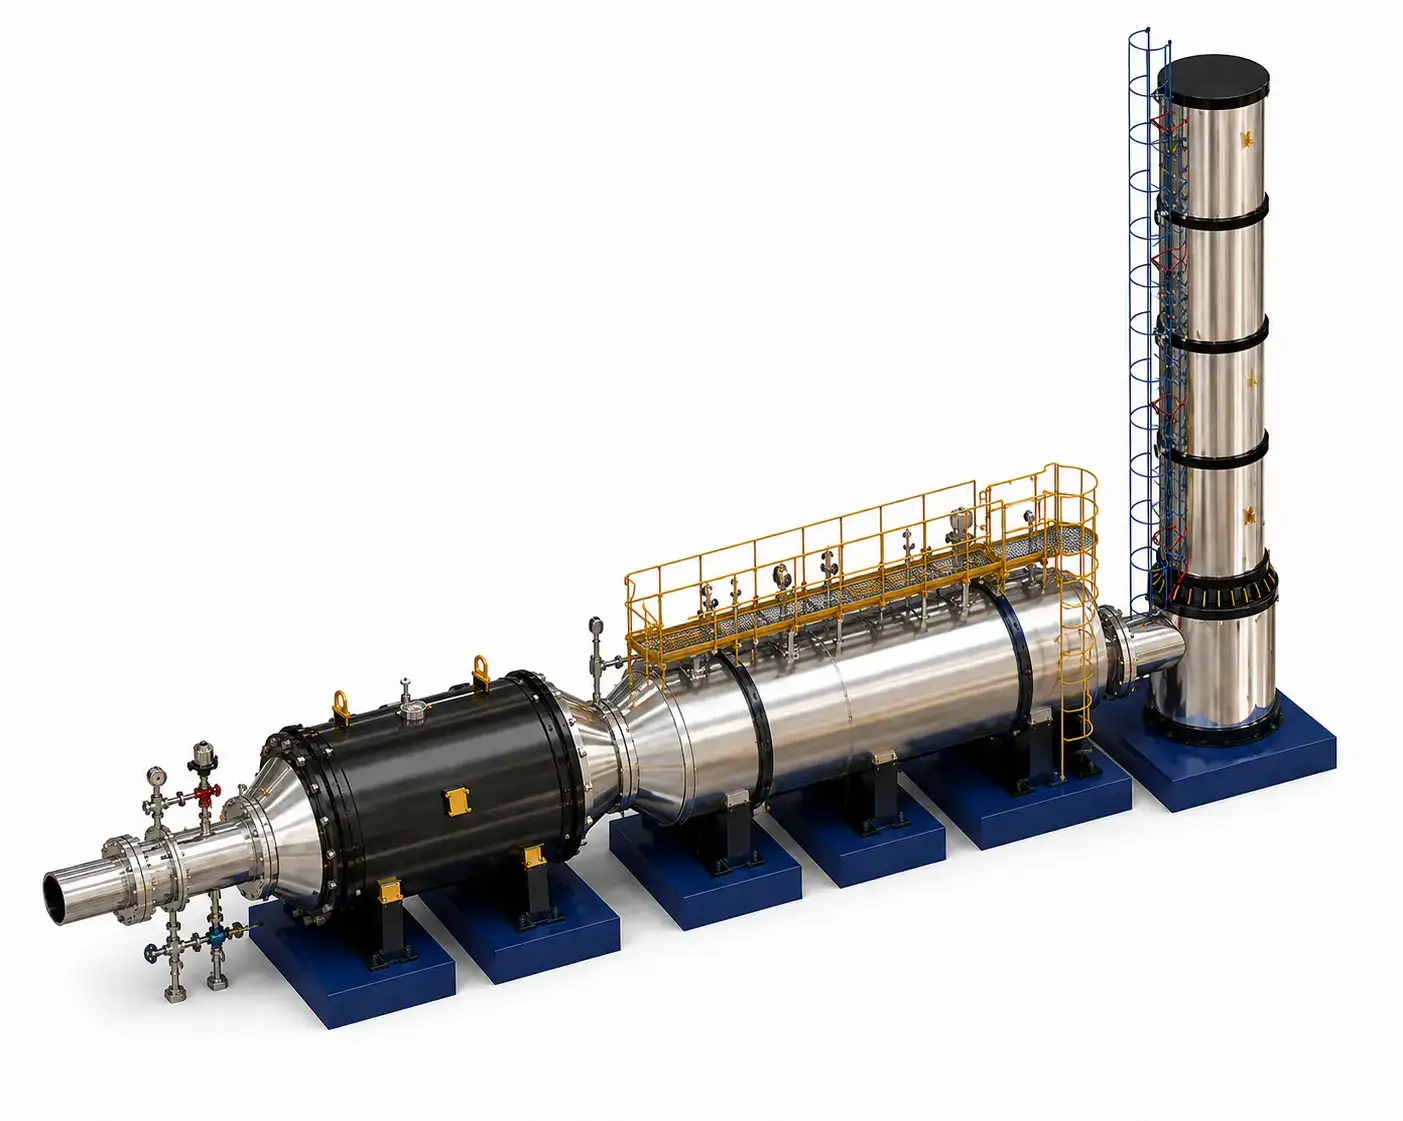
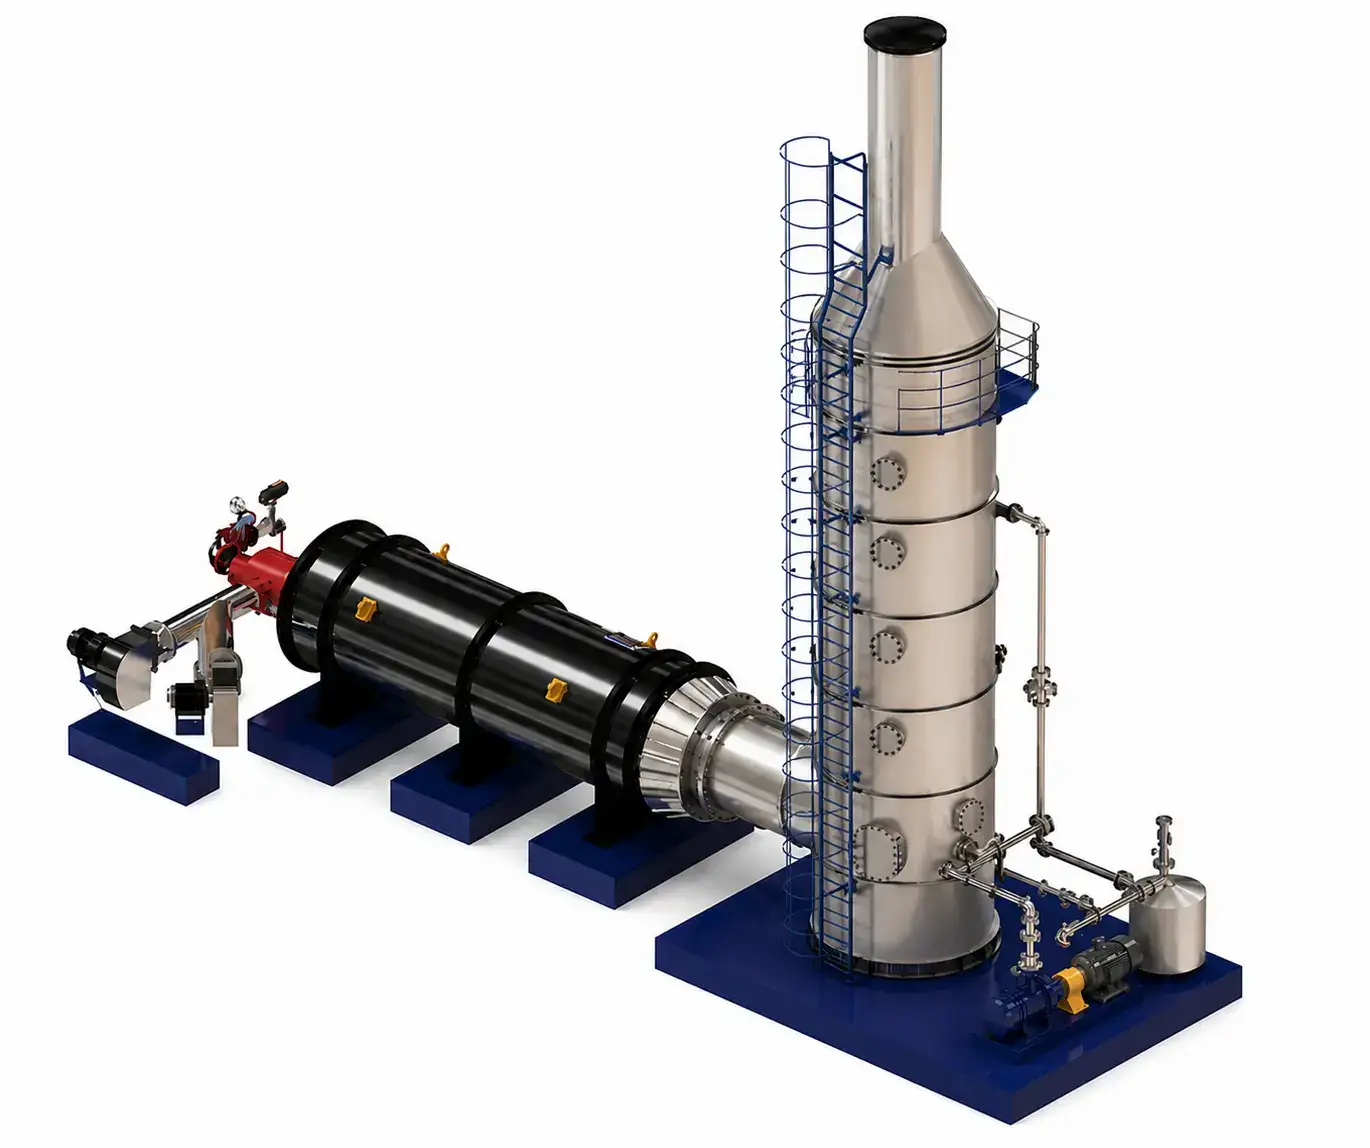
CRA's sulphur tail gas thermal oxidisers convert the hydrogen sulphide, carbonyl sulphide and carbon disulphide left after the Claus stages, with destruction efficiency above 99.9%.
DRE
>99.9%
Target compounds
H₂S, COS, CS₂
Application
SRU tail gas
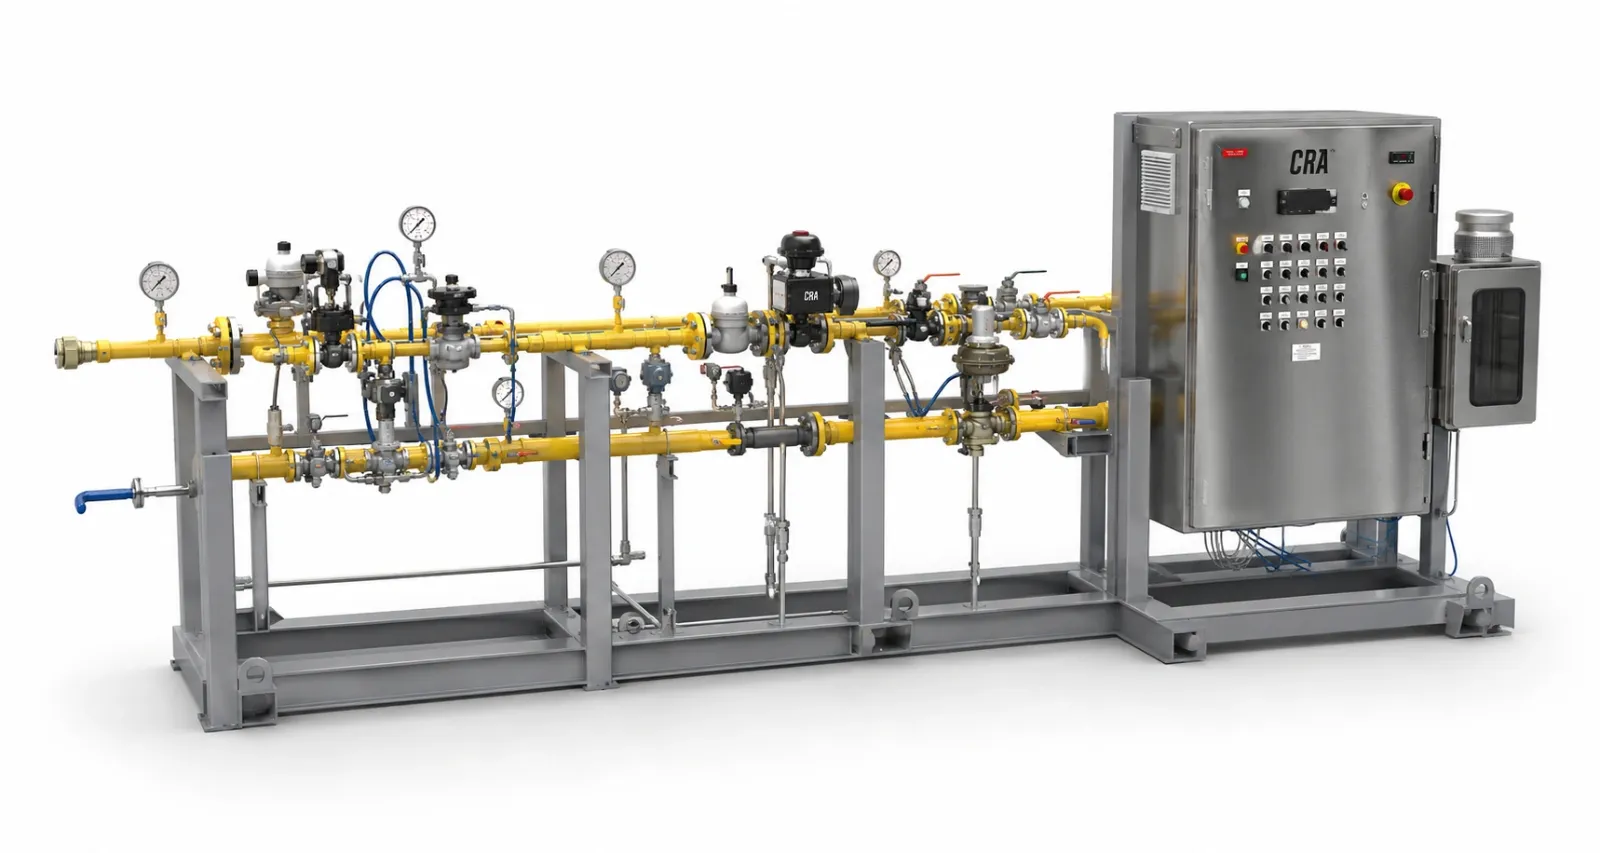
Burner management
Supplied by CRA
What does a thermal oxidiser do after a sulphur recovery unit?
A sulphur recovery unit removes most of the sulphur from acid gas, but its tail gas still holds reduced sulphur compounds. A thermal oxidiser burns this gas with fuel and air at high temperature, which oxidises the remaining sulphur compounds to sulphur dioxide. The treated flue gas then leaves through the stack.
How it works
The oxidiser sits after the last Claus stage or the tail gas treating unit, ahead of the stack.
Tail gas from the sulphur recovery unit flows to the oxidiser.
The burner fires fuel gas and air to reach the oxidation temperature.
H₂S, COS and CS₂ oxidise to sulphur dioxide in the combustion chamber.
The chamber holds the gas long enough for complete oxidation.
The treated flue gas leaves through the stack.
Key Benefits
Reduced sulphur compounds are oxidised with destruction efficiency above 99.9%.
The design suits the composition and flow of Claus tail gas.
Hydrogen sulphide, COS and CS₂ are converted to sulphur dioxide before the gas reaches the stack.
CRA supplies the burner management system with the oxidiser.
Each oxidiser is designed for the plant's sulphur recovery capacity and stack requirements.
Projects That Push Boundaries

Simultaneous destruction of multiple corrosive gas streams in an active paper manufacturing process.
The CRA Edge
CRA has more than 30 years of experience in gas handling and combustion engineering.
Design, R&D and manufacturing are carried out under one roof.
ISO 9001 certified through TÜV NORD, with designs aligned with ASME, API and CE.
Designs are customised to the process needs and the regulations that apply at site.
Applications
Built to help you specify.
Sizing tools, decision guides, and technical references. Use them before, during, and after your evaluation.


Frequently Asked Questions
Why does SRU tail gas need a thermal oxidiser?
Tail gas still carries H₂S, COS and CS₂ after the Claus stages. The oxidiser converts them to sulphur dioxide before the gas reaches the stack.
What destruction efficiency does the oxidiser achieve?
CRA designs its sulphur tail gas thermal oxidisers for destruction efficiency above 99.9%.
Can sulphur pit vent gas go to the oxidiser?
In many plants it can. CRA reviews the pit vent flow and composition and includes it in the design where it is suitable.
What data does CRA need to size an SRU tail gas oxidiser?
CRA needs the tail gas flow and composition, the fuel available, the stack limits and the site conditions.
Does CRA supply the burner management system?
Yes. CRA supplies the burner management system and integrates it with the oxidiser.